SIX UK REFERENCES FOR ANTIVIRAL TEXTILES AND SPECIALIST COATINGS FOR DIGITALLY PRINTED FABRICS

“Antiviral and Antimicrobial textiles are a specialist field, but nevertheless a sector which we must now all explore to maximise NEW opportunities for the print industry.”
Antiviral fabrics are in demand. As we emerge from the current global health pandemic, the fabrics that once typically adorned Medical environments and Care Homes are now required in order to protect the workplace, leisure industries and all public spaces.
Textiles with inherent woven antimicrobial fibres or surface treatments offer varying degrees of protection and seek to reduce the possibility of cross-contamination.
With a wide variety of end-uses these fabrics which were once only specified for medical and healthcare interiors are now in demand and becoming multi-disciplinary.
Whether you are looking for fabrics for Home Furnishings, Interior products or even Apparel many of the substrates and fabric coatings used in the contract space can be utilised beyond their original purpose.
Contract furnishings is a sector ahead of the curve for antimicrobial and antiviral textiles and offers a myriad of fabric choices for potential new applications. Typically, these fabrics are often also fire-resistant as specified for contract use. Fabrics are also durable and built for heavy use and wear and tear. These textiles are now in demand for residential and even apparel use.
Here’s a snapshot of UK Textile suppliers and Specialist Coating companies that supply bases and / or coating services to the Digital print sector:
Edmund Bell (Contract Textile supply and Printing)
Edmund Bell is a leading global supplier of fabrics and accessories to the commercial, institutional and domestic interiors markets; offering design-led technical expertise, support and service to designers, specifiers and contractors in the hospitality, leisure, healthcare and education sectors.
Carrington Textiles (Apparel Textile Supply)
The largest producer of workwear fabrics in the UK, exporting to more than 80 countries worldwide, with over 60% of our products going to new markets. Produce over 55 million metres of fabric annually.
Based in Lancashire, with over 125 years’ experience of textile processing and finishing. This is supported by massive investments in one of Europe's largest fully integrated textile processing and finishing operations. Specialising in the development of fabrics and finishes with exceptional performance in the most demanding workplace environments.
PANAZ (Textile Supply & Shield Plus topical spray coating)
As global suppliers of anti-microbial fabrics for the healthcare, Panaz are acutely aware of the need for textiles which effectively prevent the spread of infectious diseases in hospitals, care homes and other environments where vulnerable individuals may be exposed to potentially harmful pathogens. As such, they have taken the proactive measure of independently testing Shield Plus™ Anti-Microbial technology against the spread of the coronavirus strain, to reassure customers of the effectiveness of Panaz products against the rise of new contagious diseases.
Whalleys (Textile supply and coating)
Whaleys Bradford offer a wide range of over 450 fabrics, which include natural (loom-state) cottons, silks, linens, jutes and wools, many of which are specially prepared for dyeing and/or printing.
They also stock a large selection of coloured Silesia cottons, mixed fibres, synthetics and even speciality fabrics manufactured from bamboo, banana, pineapple or soyabean fibres and offer a specialist coating service subject to your requirements.
ALLTEX (Coating)
Alltex Ltd are a small company situated in Tottington, Bury, Lancashire.
The main core business is commission beaching and dyeing. However, they also prepare fabrics for Digital Textile Printing. Offering bleaching and pre-coating of fabrics, so that they are ready to be digitally printed. Alltex also bleach, raise, emerise, calender and finish cloth for customers adding specialist coatings when required.
EUROFLAM (Coating)
With a combined 40 years + experience in textile treatments, and with a capacity now in excess of 1 million metres a year. Euroflam offer a very wide range of treatments, Flame Retarding, for both Domestic & Contract uses, Water Proofing, Soil & Stain and Anti-Microbial and several others as required.
Antiviral fabrics are in demand and offer the print community new opportunities…
Colour Is Too Important to Leave to Chance
Print will always be the part of the garment people see first.
But the sum of all parts — the fabric, the trims, the fasteners, the finish — is what determines whether a design actually delivers on its promise. Brands that continue to treat colour as a single creative decision, rather than a coordinated technical discipline spanning their entire supply chain, will keep paying for it in re-dips, delays, and disappointed design teams.
A Century of Textiles, and an Ever-changing World
Few companies can trace their roots back more than a century and still count themselves among their industry's innovators. Texia, headquartered in Monistrol de Montserrat, Spain, is one of them.
But the story of Texia is not simply one of longevity.
It is a story of continual reinvention. As the textile industry has grown more global and competitive, Texia has repeatedly reshaped its business, investing in technology, developing its own brands, and placing sustainability at the centre of its mission. In doing so, it offers a compelling example of how a heritage manufacturer can lead rather than follow through a period of profound industry change. Image Credit: Texia
What are we craving Ultimately?
The instinct to slow down while simultaneously optimising every measurable aspect of life isn't a passing curiosity. It's a structural response to a world that feels increasingly unstable, and it's reshaping what people expect from their homes, hotels, workplaces and healthcare environments alike.
For the design and manufacturing sectors, this means rethinking both product and process.
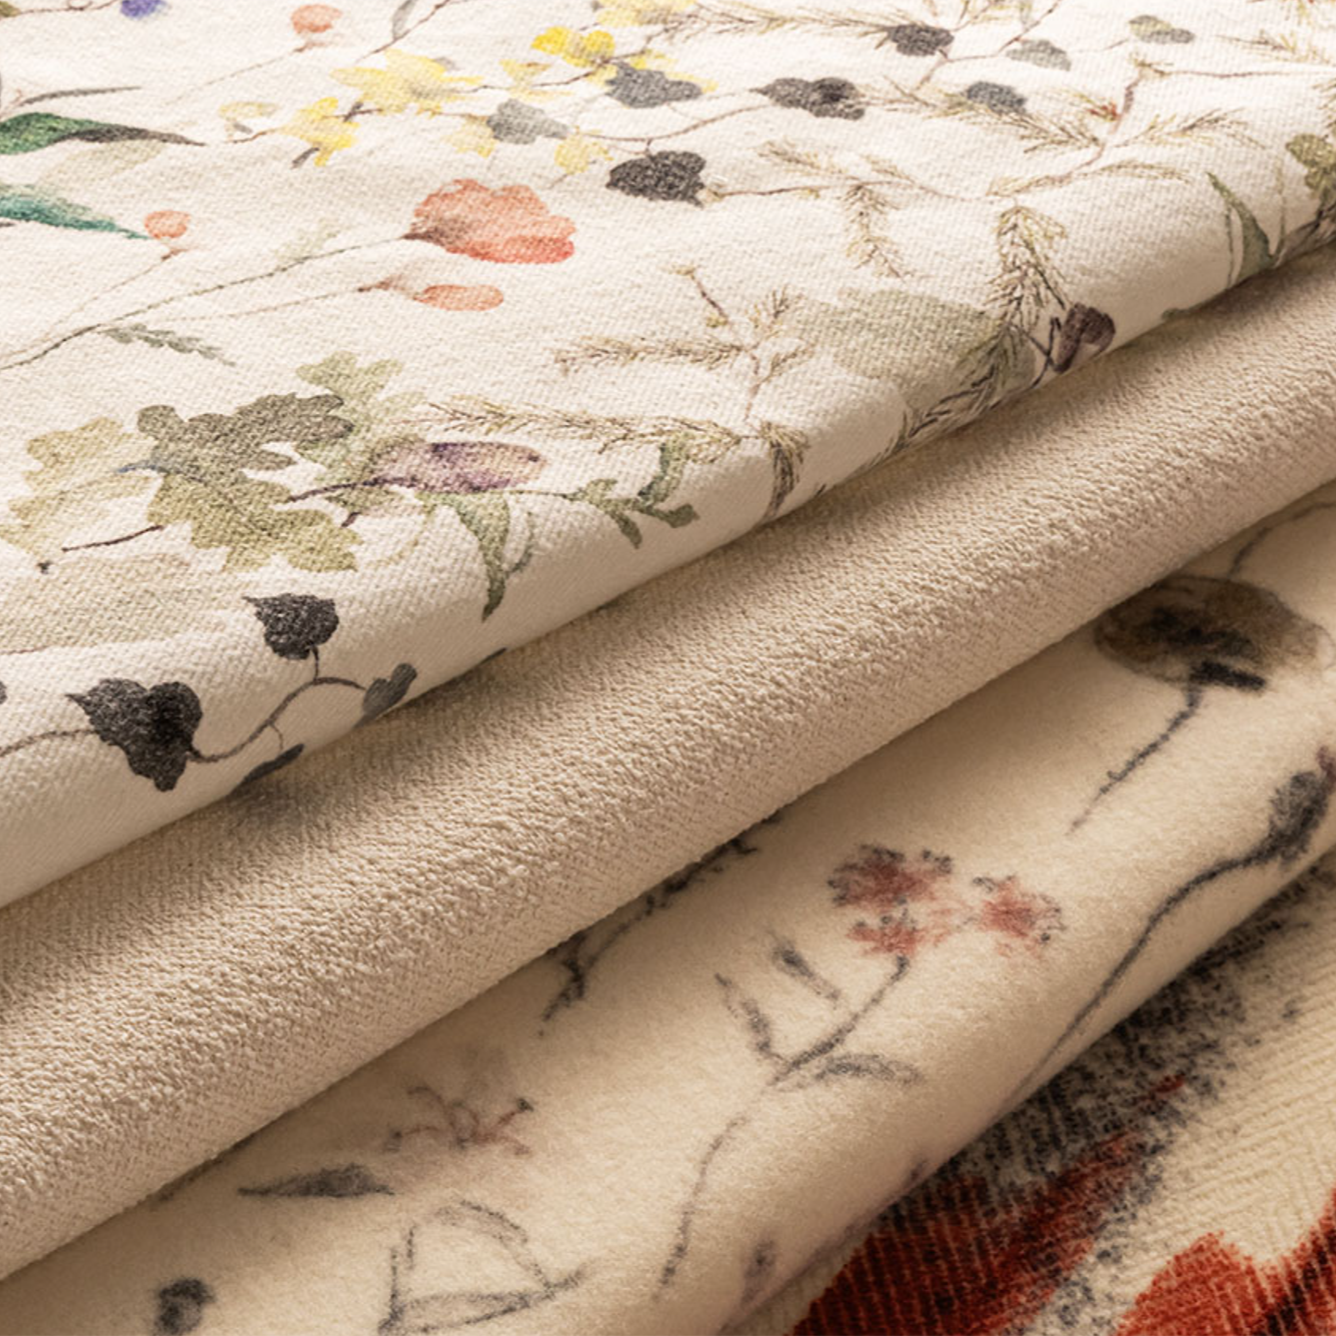
The Structual Shift is Real and its Already Here
Volumes are moving east, where digital production is accelerating rapidly. Consumer behaviour has shifted.
Demand is now driven by personalisation, shorter buying cycles, and an expectation of near-instant responsiveness. Regulatory pressure is intensifying, with supply chain transparency now a legal and commercial fact in many markets. And margins? They are under sustained, structural pressure.
This is not a temporary disruption. It is a fundamental reordering of how textile manufacturing must operate.
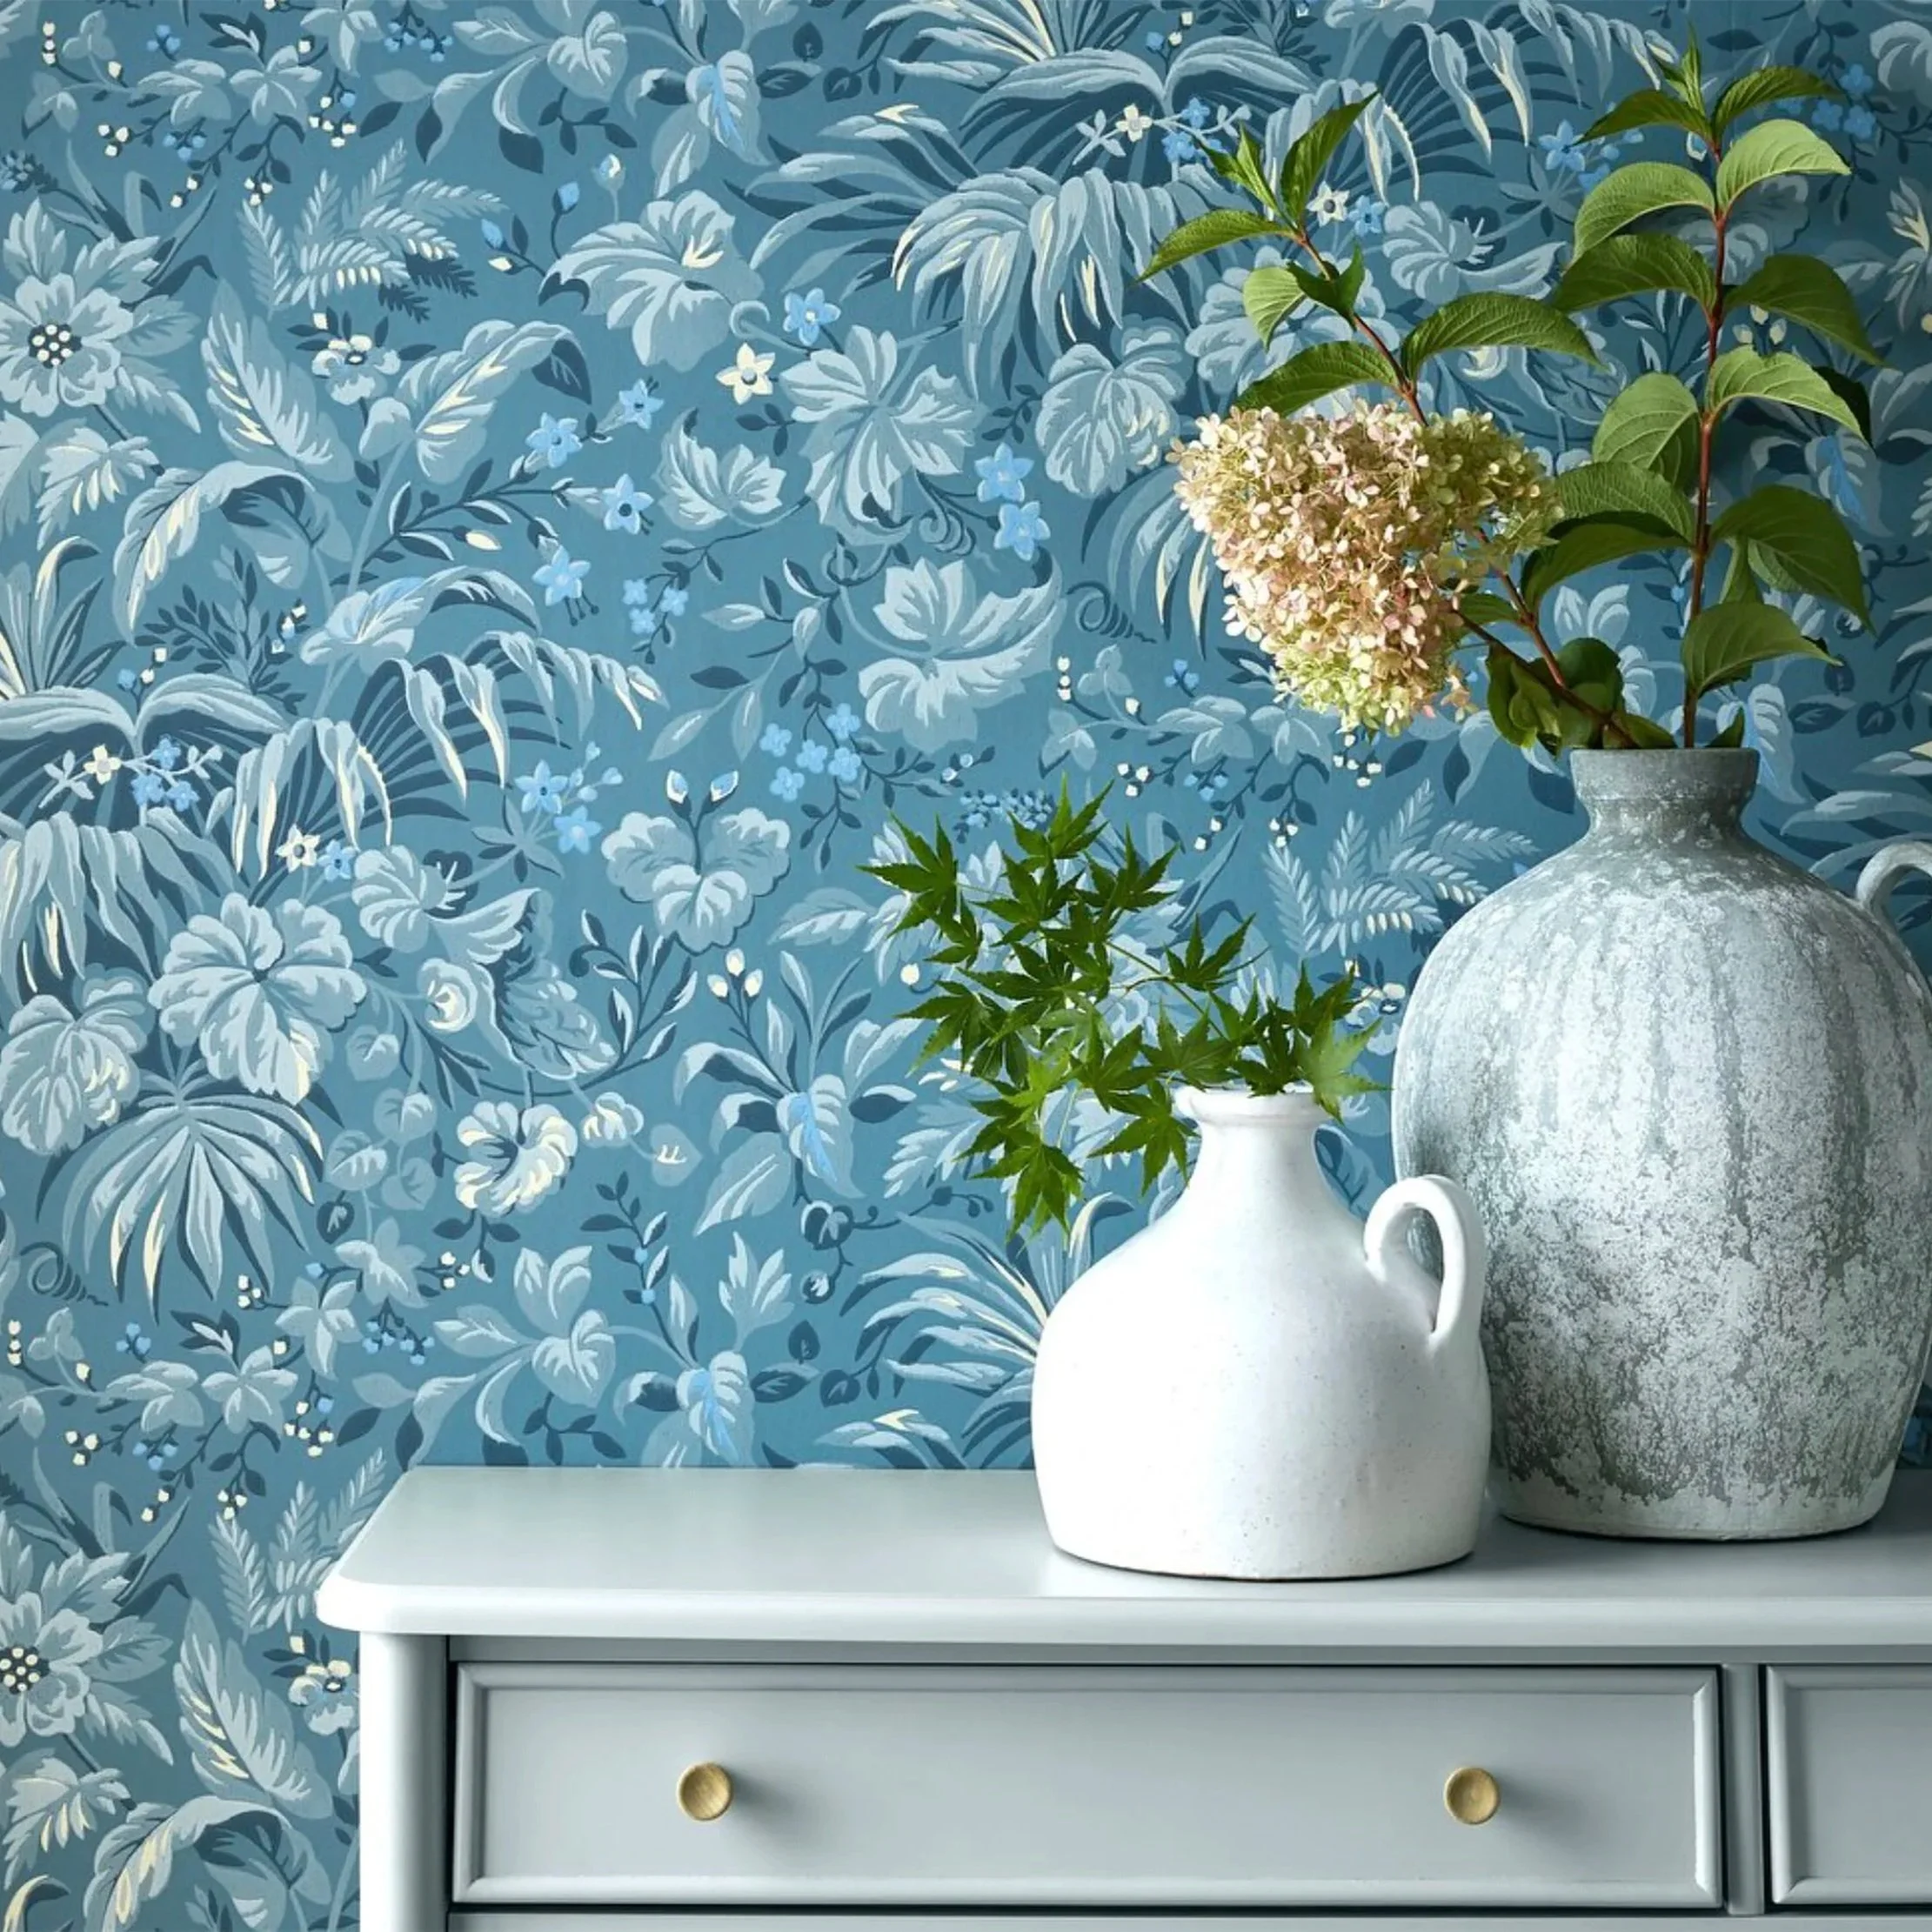
The Challenge: Standing Firm as the Industry Shifts
The wallpaper landscape has changed dramatically. Digital printing has lowered the barrier to entry, spawning countless direct-to-consumer brands and pushing much of the market towards faster, cheaper production.
At the same time, manufacturing in the UK has grown steadily harder - rising minimum wage, national insurance, energy and substrate costs all bear down on margins. Surface Print have embraced all of these challenges - and stand resolutely prepared for the future.
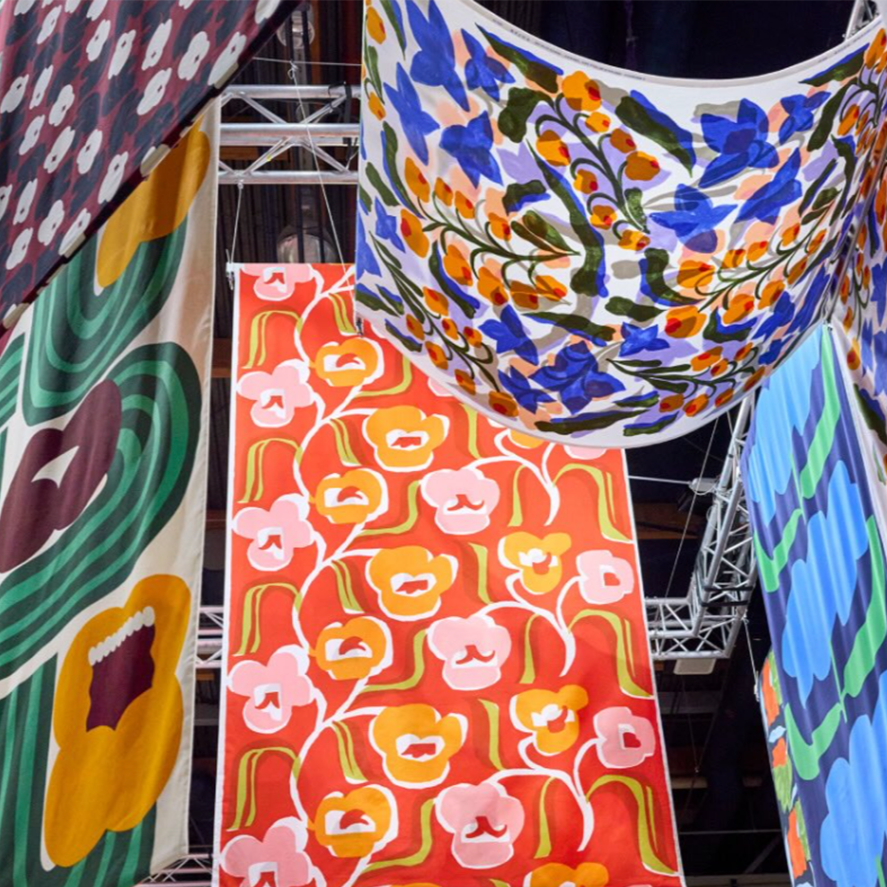
From Helsinki's printing mill to Paris's Le Marais, discover how Marimekko is scaling a design-led brand with purpose, craft, and bold innovation.
But what makes Marimekko's story compelling is not just its aesthetic legacy?
The word "toxic" carries weight. It conjures danger, harm, and things best avoided.
“Yet in the textile industry - Where between 3,000 and 10,000 chemicals move through the supply chain, a reflexive fear of the term is one of our biggest obstacles to progress.”
This article distils the key takeaways and what buyers, designers, and brands should be asking right now.
What Is the Digital Product Passport?
At its core, a Digital Product Passport is a digital record attached to a physical product - For a printed textile product, this means the DPP would capture data on the substrate, inks and dyes used, the printing process and technology, chemical compliance, environmental impact (including water and energy use), supply chain traceability, and end-of-life instructions.
The Market Gap that Changed Everything
Future Fashion was founded in 2019, timed deliberately to coincide with a pivotal moment in global textile technology: the commercial launch of the EFI Reggiani BOLT Single-Pass digital printing system.
The founders recognised that single-pass architecture had fundamentally changed what was industrially possible - and that Pakistan's domestic market had yet to catch up.
Print is no longer defined by the inefficiencies that once characterised it…as advances in production processes and technology have significantly improved its environmental performance.
Taran Rai, Corporate Sustainability Manager at Epson explains why?
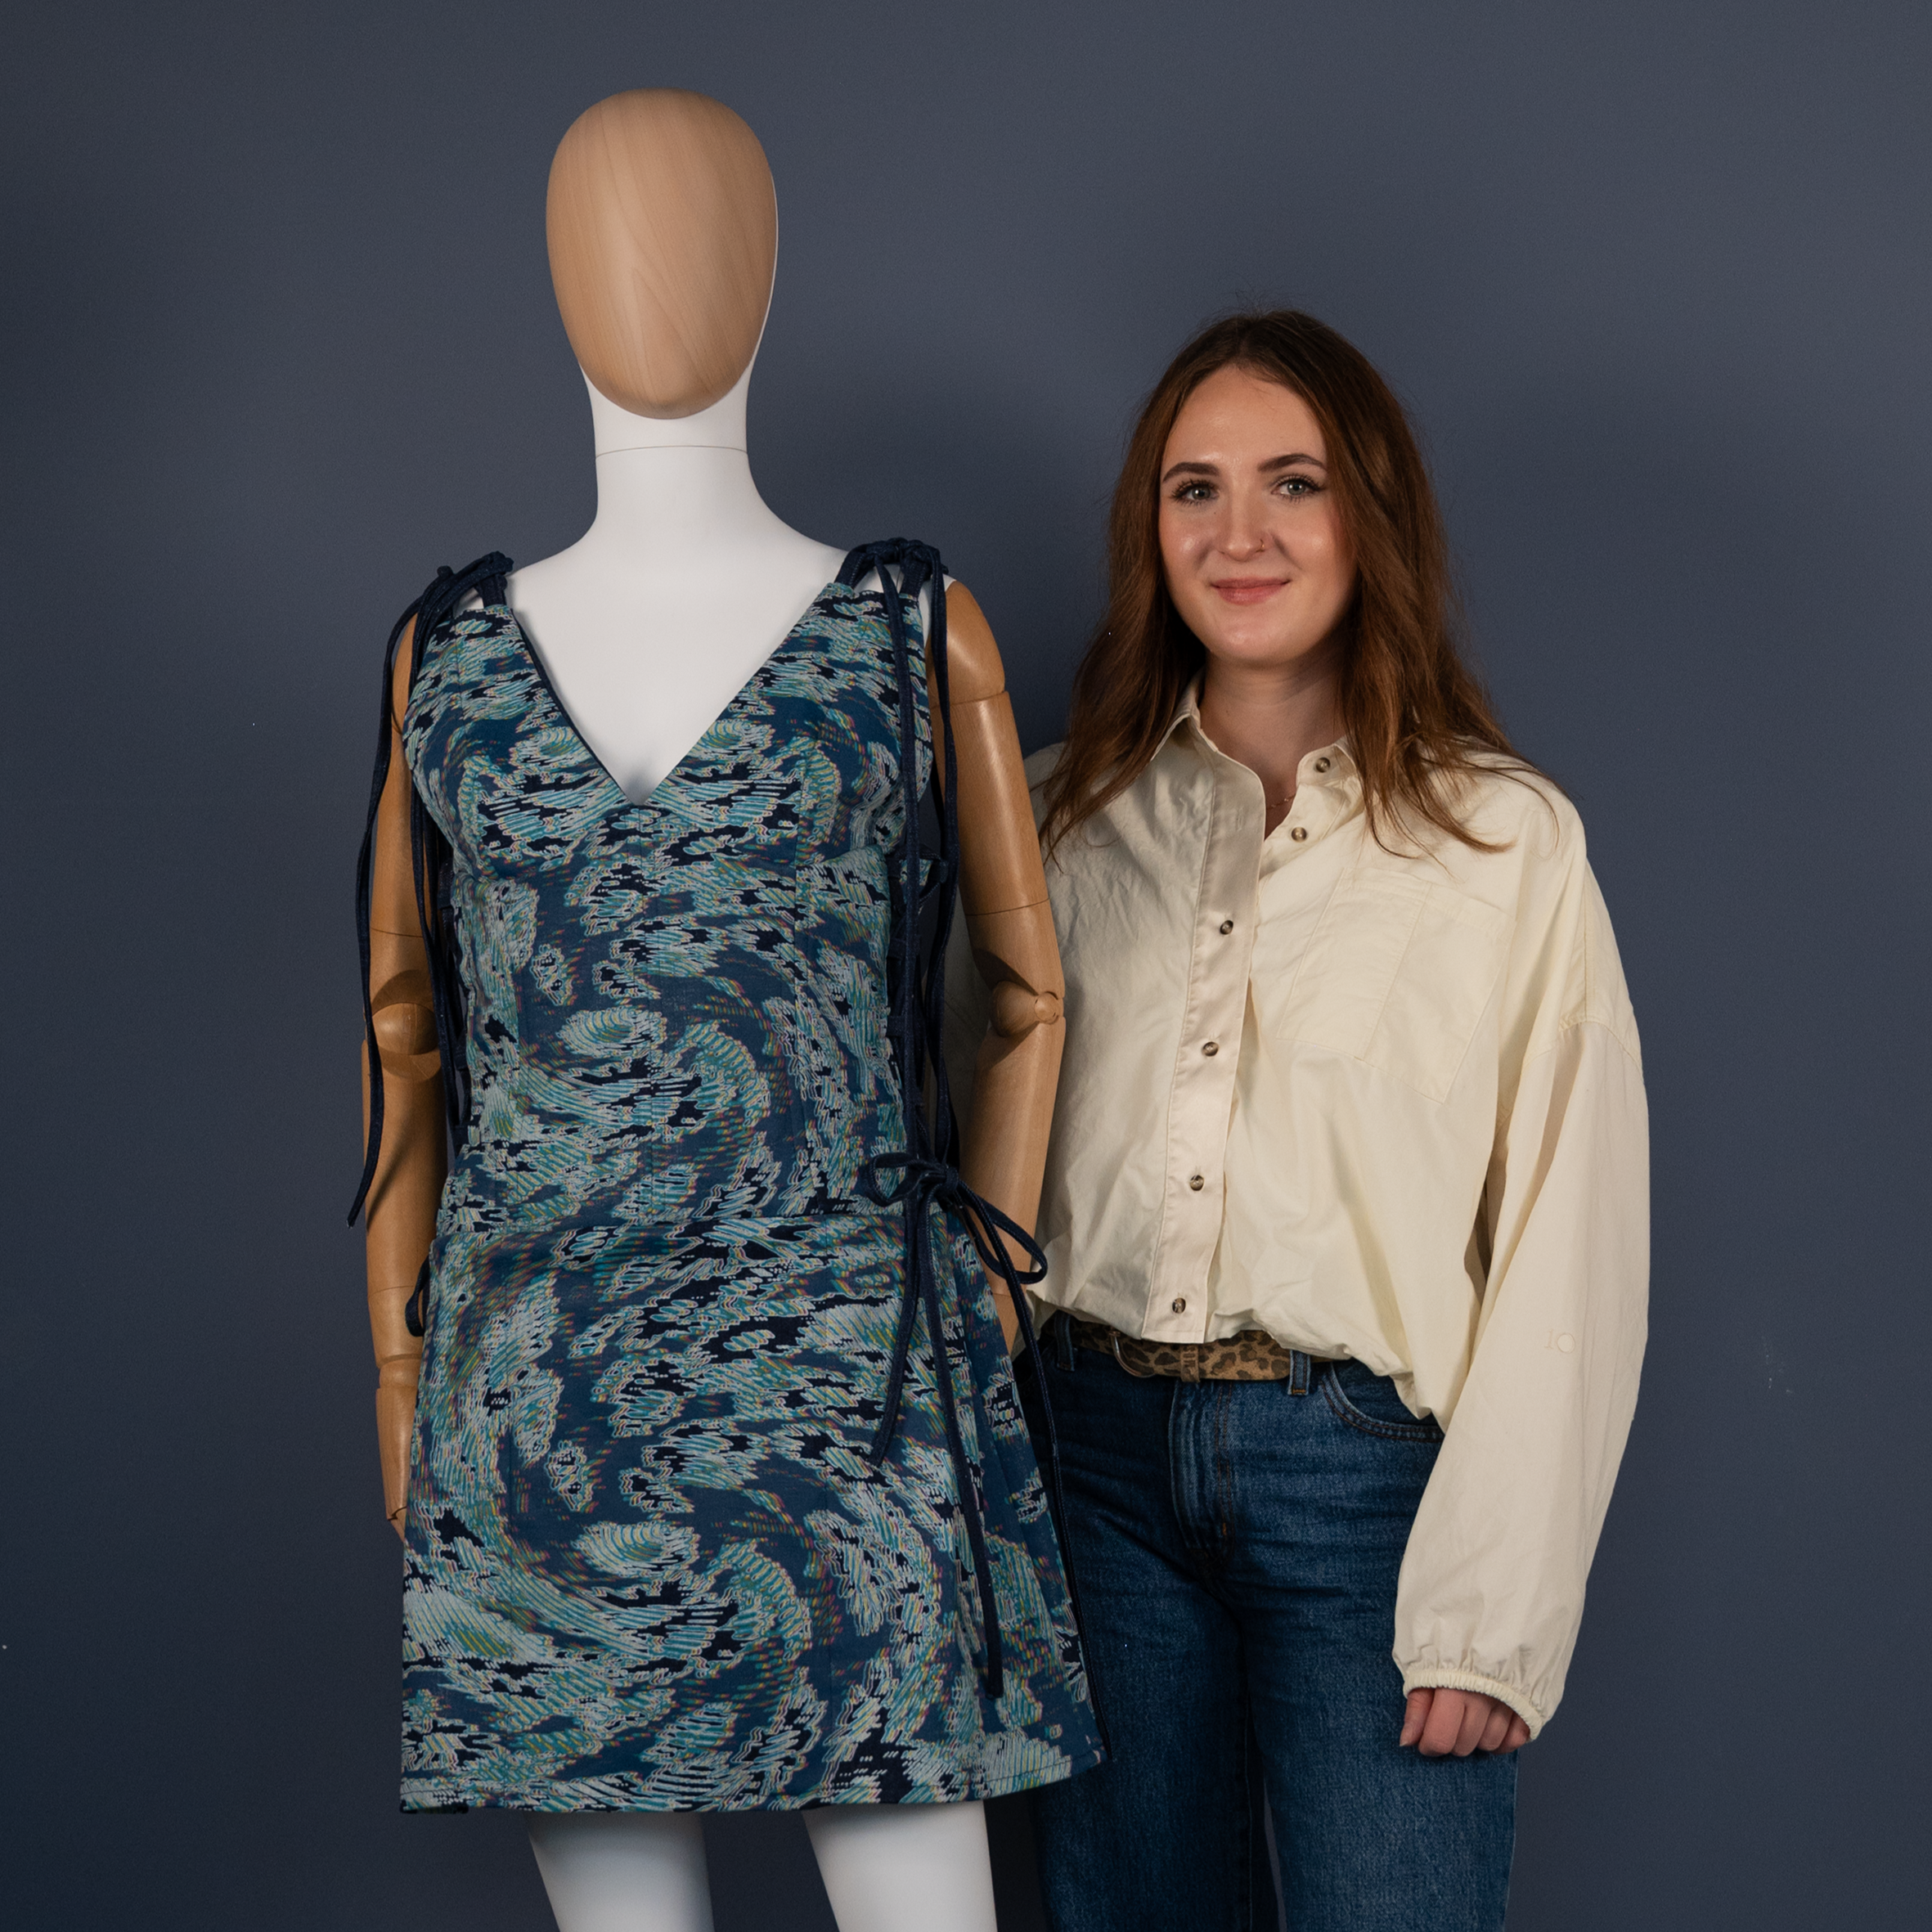
The story of what happens when young designers access digital technology is still being written.
What once was a theoretical sustainability goal seems to have shifted into an active regulatory reality.

Is the Textile Market Finally Recovering?
After a difficult few years, there are genuine reasons for optimism. Duncan was candid about the challenges: "The market for textiles has been very difficult over the last three years. I'm not going to hide the truth there. But the tide is turning.“
A profound shift is currently reshaping the sector
Changing consumer expectations demand greater design diversity, faster turnaround times, and sustainable manufacturing practices.
To thrive, interior brands must adapt their supply chains, bringing production closer to the end consumer and moving away from bulk manufacturing.
Digital textile printing offers a definitive solution to these operational bottlenecks.
Digital transformation doesn't announce itself.
It accumulates - one innovation at a time - until an entire industry looks back and realises the ground has shifted beneath its feet. That's precisely where textiles stands today.
The conversations happening now about AI, automation, sustainability, and digital product passports are not theoretical. They are shaping decisions being made on factory floors and in boardrooms right now.
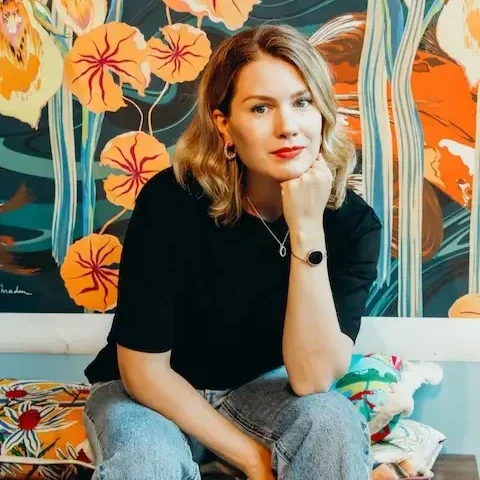
“By leveraging advanced digital textile printing, Marylene Madou has successfully merged traditional craftsmanship with cutting-edge technology. Her approach offers a blueprint for how independent designers can scale their brands globally while maintaining a minimal environmental footprint.”
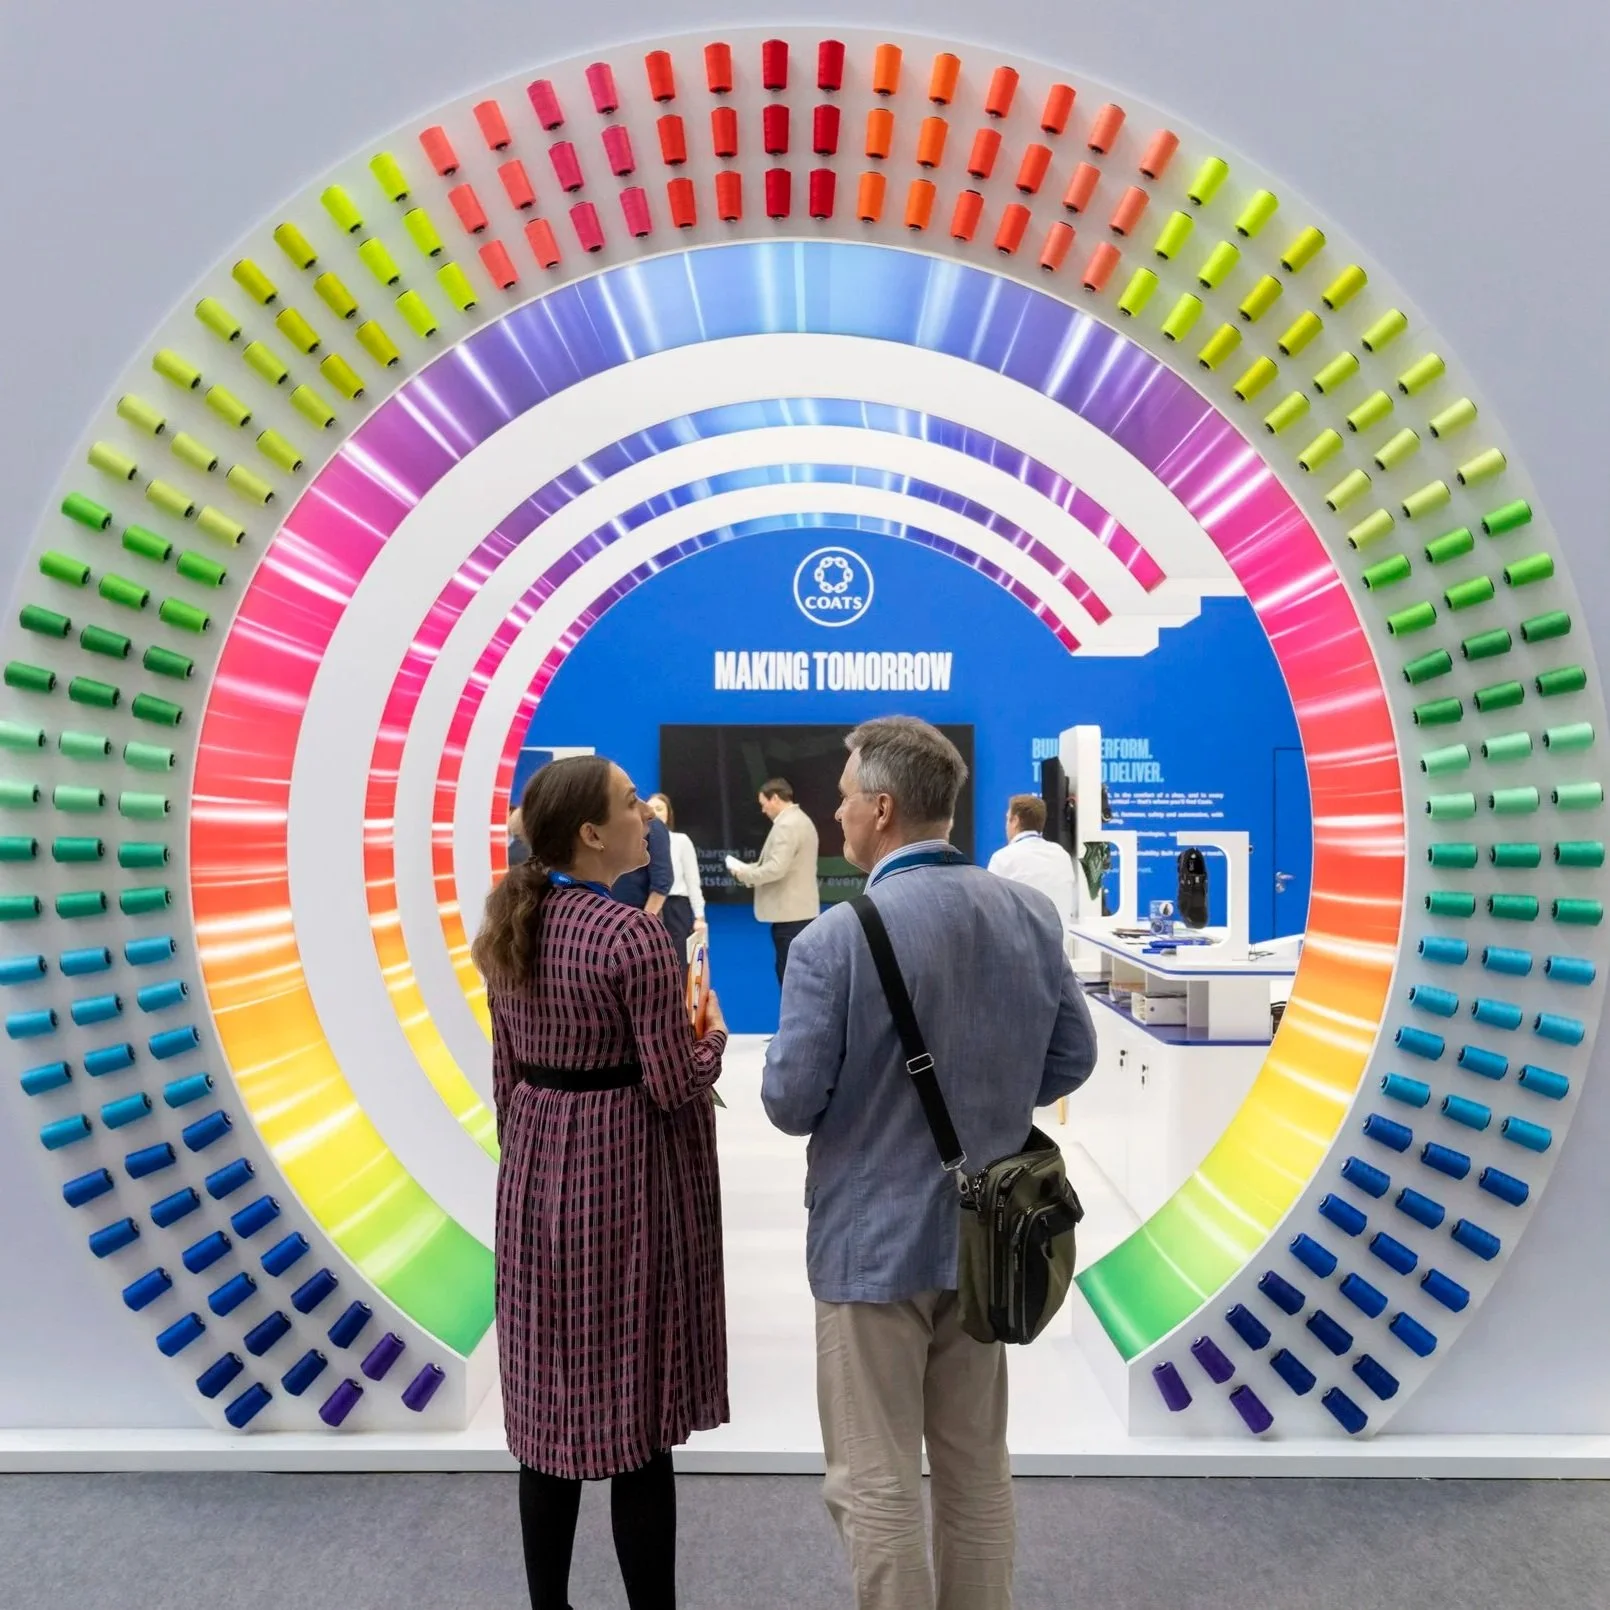
The textile industry is undergoing a vital transformation. As the insights from Techtextil and Texprocess reveal, the path forward relies on a combination of sustainable hardware, intelligent chemistry, and seamless digital workflows.
From Zimmer's industrial-scale energy reductions and Stratasys's on-demand 3D embellishments, to Kornit's single-step technical printing and the unified digital ecosystems of NedGraphics and Optitex, the tools for change are here. To stay competitive, brands and manufacturers must adopt these innovations, moving away from fragmented, wasteful processes towards a truly connected, circular economy.
Friedmans stands as a testament to the power of combining traditional textile knowledge with forward-thinking innovation.
“Operating from their UK headquarters, Friedmans now serves a diverse array of sectors, including swimwear, dance, entertainment, sportswear, interior decor, prosthetics, and even pet apparel. With a strategic supply chain that reliably serves clients worldwide”
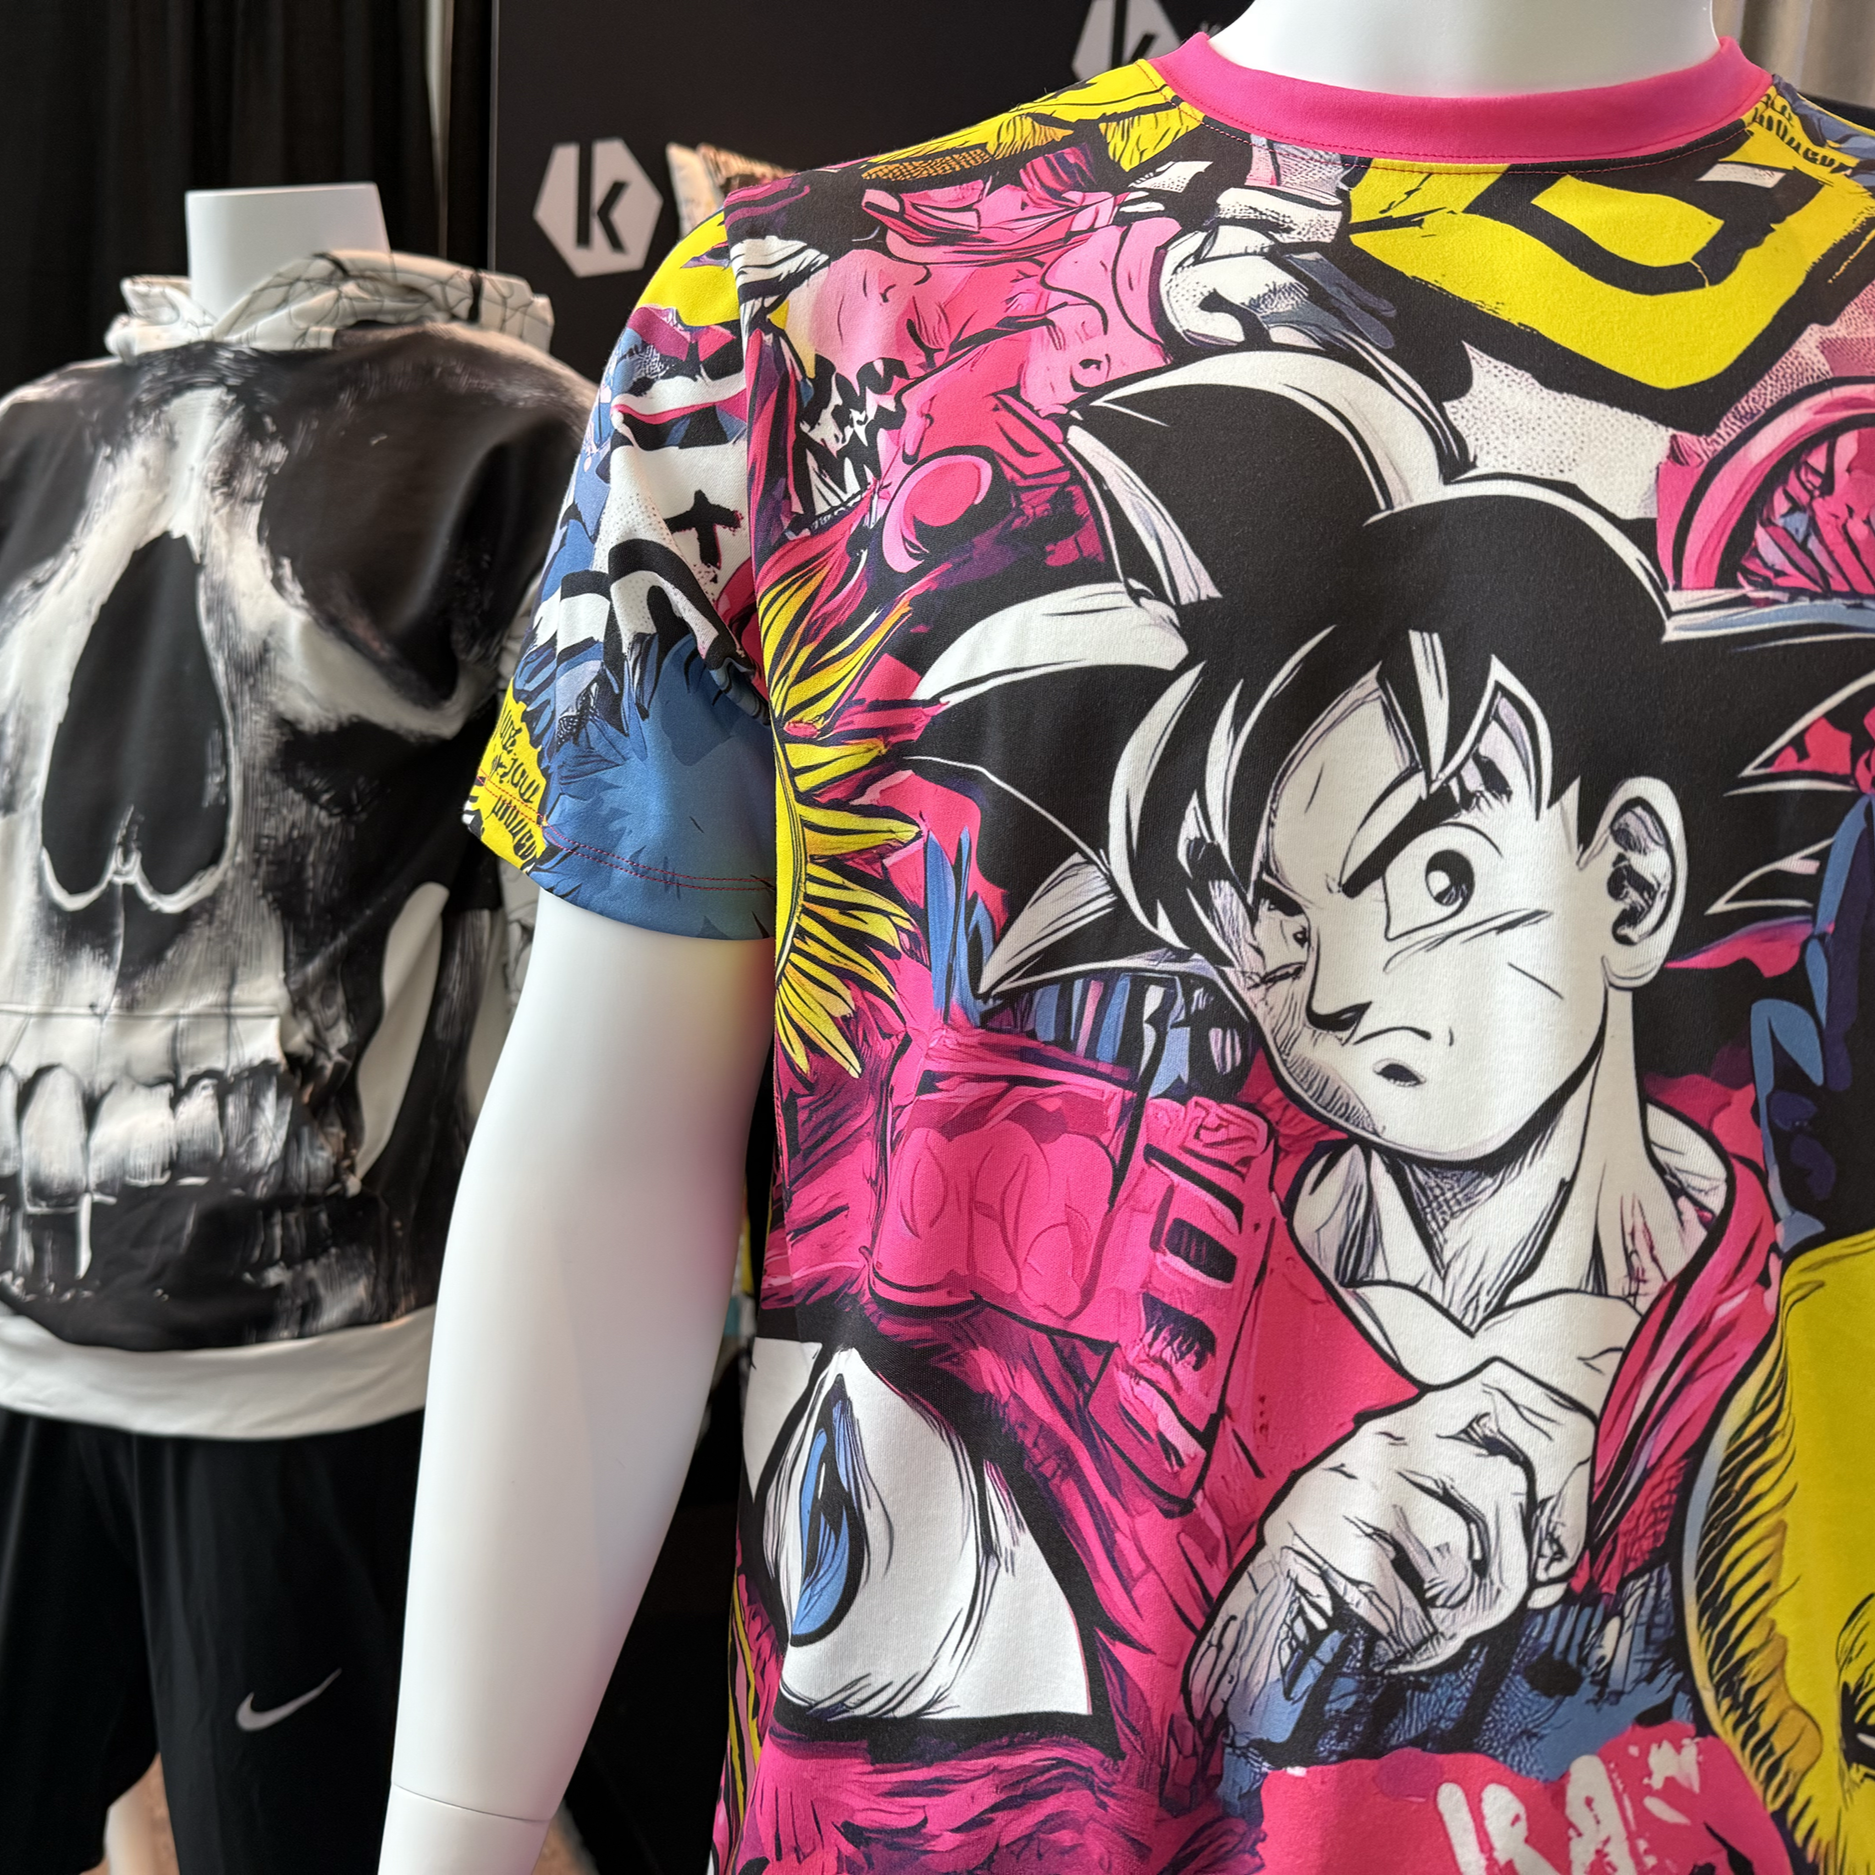
The apparel decoration industry is decisively moving away from isolated, analogue production tools toward connected digital manufacturing environments.
"Kornit’s unwavering commitment to transformative technology continues to disrupt the status quo. For business leaders and innovators ready to capture the future of apparel manufacturing, the path forward is clear”
The Urgent Need for Sustainability at Scale
The transformation at Coats provides a vital blueprint for the wider textile and apparel sector. True sustainability cannot be achieved in silos. As Dearing emphasised:
“Cross-industry collaboration is the engine of meaningful change. Brands, machinery suppliers, chemical providers, and fibre producers must act as an interconnected ecosystem”
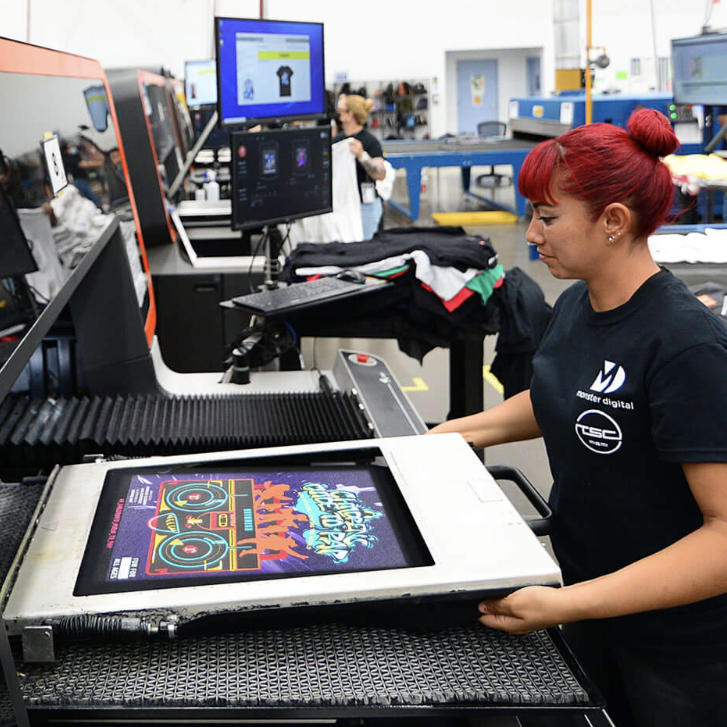
Today’s customers demand superior product quality, real-time data visibility, and lightning-fast turnaround times.
For large-scale garment decorators, managing these expectations while balancing seasonal demand fluctuations - such as the massive surges seen during Black Friday - presents a monumental challenge.
"Relying on transactional vendor relationships and outdated legacy equipment is no longer sufficient to secure long-term stability and growth.”
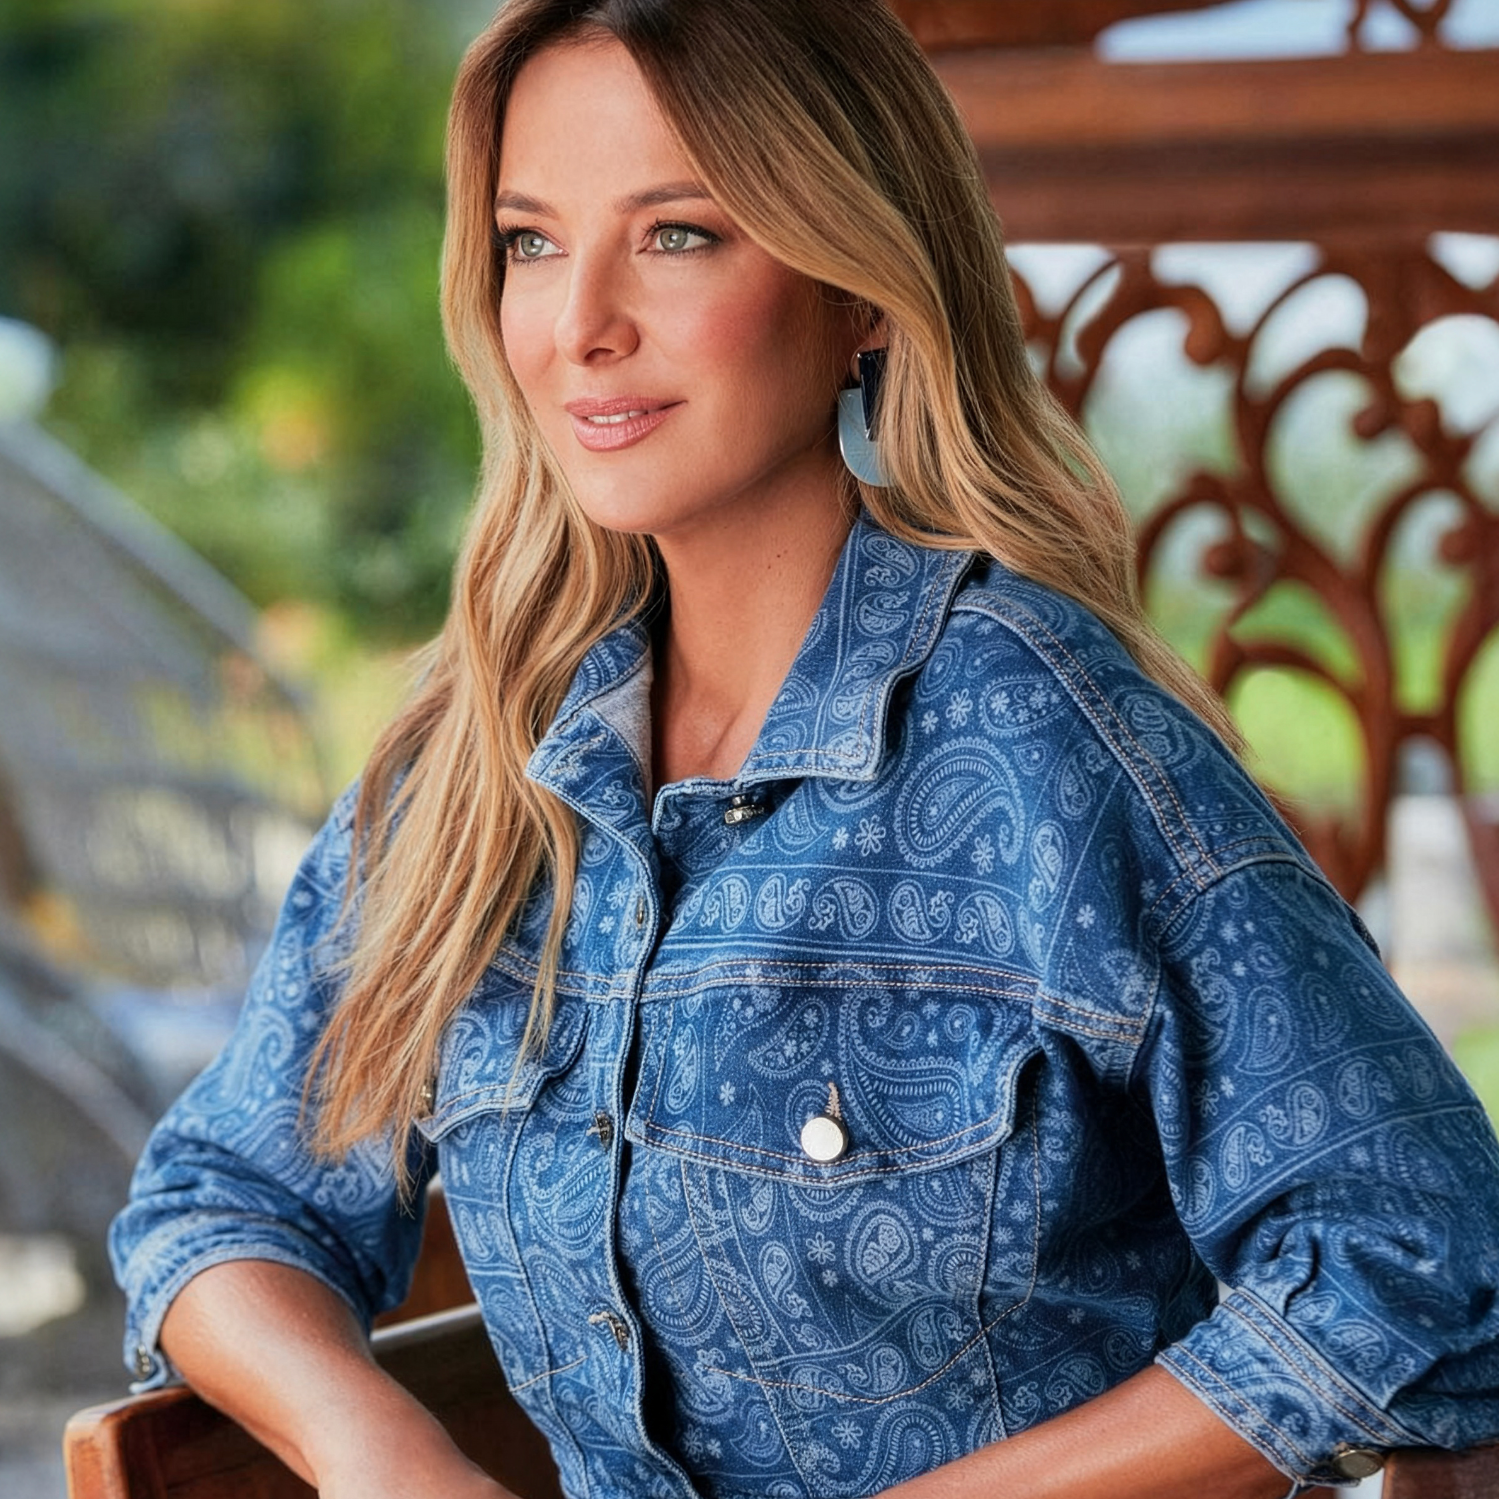
Printing method is never a secondary detail. It shapes the entire life cycle of a product, from concept to customer. In today’s fashion industry, where margins are tighter and speed matters more than ever, technical knowledge has become a competitive advantage.
“The future of textile design belongs to professionals who can combine creativity with execution, aesthetics with practicality, and vision with production reality”.
Friedman’s is a UK-based wholesale specialist. Offering stretch textiles, digital print & foil effects, supplying designers and brands worldwide.
FabricVision is a fresh, dynamic player in the large-format digital textile printing industry. Backed by over 100 years of combined expertise, we offer a fully integrated production model.
With over 40 years of textile expertise, Greentex leverages a global portfolio & presence to serve a diverse range of fast-to-market customers.

Premier Digital Textiles has been the leading supplier of fabrics ready for printing for over 30 years.