HOW HYBRID DIGITAL TEXTILE PRINT TECHNOLOGY IS UNLOCKING THE TEXTILES VALUE CHAIN

“Technical innovations and entrepreneurial business models are driving this reform, as machine manufacturers come up with more hybrid functions for their offerings - all of which push production costs down and meterage volumes up” - TEXINTEL
How Hybrid Digital Textile Print Technology Is Unlocking The Textile Value Chain
IMAGE CREDIT: DURST GROUP
The global digital textile printing machine market was valued at $175.4 million in 2017, and is expected to reach at $392.3 million by 2025, growing at a CAGR of 10.4% during the forecast period. (Allied Market Research)
Factors such as an increased awareness of sustainability and the impact of traditional textile production and its contribution to greenhouse gasses alongside the continued rise of fast-fashion and its requirement for on-demand-production, the growth in per capita income of individuals, and a surge in demand for short run products driven by the consumers desire for design diversity and customisation.
All these factors have driven the global digital textile printing machine market forward.
Many now believe that the markets growth will be further accelerated by the impact of COVID-19 as the textile supply chain struggles to survive in its current format - with a step-change to localised production now predicted my many experts.
Digital Textile production offers a viable solution to reverse legacy pollution.
The energy efficient, clean technologies utilised in digital textile production are boosting the global digital textile printing machine market growth. In addition, stringent government regulations for reducing pollutants alongside ethical manufacturing supplement the digitisation of the Textile industry.
The direct-to-fabric segment accounted for more than half of the market share in 2017 and is expected to witness significant growth during the forecast period (Allied Market Research).
Technical innovations and entrepreneurial business models are driving this reform, as machine manufacturers come up with more hybrid functions for their offerings all of which push production costs down and meterage volumes up.
The textile industry was originally built for volume, but the landscape has changed. Solutions are now required to deliver print at all speeds in order to service this fast-evolving marketplace.
The fastest digital printing machines are the super-fast single pass printers built for high speed industrial production:
Here, the print bar carries hundreds of single print heads, the carriage is fixed over the fabric and doesn’t transverse the width of the machine, the only moving component is the fabric itself.
The result of this particular Hybrid application is a step change in print speed, with machines such as the EFI Reggiani Bolt producing at over 5,400 metres per hour followed closely by the MS Lario on 4,500 metres per hour and the Spg Prints Pike machine on 2,400 metres per hour.
These machines require a significant investment but also demand minimum production volumes in the many millions of metres per annum to guarantee a decent return on outlay and assured profits.
Down the scale from these are the medium industrial speed (300-600 metres/hr) machines where hybrid functions have introduced quality and production improvements that create true versatility and create the basis of the Digital Textile Micro-Factory.
Simplifying the print process is the Kornit Presto, whose hybrid functions include in-line per-coating, in-line softening and in-line curing.
This one-step process is achieved through the use of inkjet heads being used to apply the pre-coating before printing and the softener after printing during the same pass through the machine.
The product is then cured in-line, and the result is a professionally prepared, printed and finished fabric ready to be cut and sewn, all achieved within the space of a few square metres.
These hybrid functions on the Presto, used as they are, with Kornit’s Neo-Pigment Inks, are capable of printing and finishing across the widest range of fabrics from cottons to polyesters to silks and to poly-blends, giving versatility and speed to the Digital print Process.
Similarly, at Durst, with their Alpha 350, their development of hybrid inks, called ‘Advanced Digital Pigment Ink’ has created a print environment where pre-coating and post finishing are a thing of the past on many fabrics.
Equally, with excellent fastness results on both the Kornit and Durst systems, clients can be comfortable that their choice of process meets the performance specifications of their marketplace.
Going down a gear, in speed not quality, to the so-called ‘entry level’ machine group
A recent hybrid development at Mimaki has introduced the ultimately flexible TX-300P-1800B machine, where it is possible to print with two ink sets, for example, Dyesub and Pigment on the same machine.
This gives the smaller print service provider a true advantage of being able to extend his printed textile range within the scope of a single machine, providing an efficient and cost-effective solution to what has been a perennial problem for the smaller printer.
Finally, under the heading of ‘Reinventing Dyesub’
Comes the HP Stitch with a host of innovative hybrid functions that add value and versatility to performance and quality in digital textile printing.
Starting with its built-in spectrophotometer that guarantees first time colour matching as well as consistency of colour reproduction on re-prints, the Hp Stitch brings a host of innovative hybrid features to the digital textile print arena. This front-loading machine saves space in operation, and uses HP Smart colour for Pantone emulation with a unique drop and dry system enabling the lightest papers to be used, and with its unique hybrid operating system, HP Print Os Plus can be left to print unattended for 24 hrs.
The innovation that has driven machine manufacturers to explore hybrid applications of their base technology, has created an environment where unlocking the textile value chain is a matter of scale versus speed.
It’s these developments that will nurture the growth of the sector and further unlock commercial opportunities within the textile industry.
Colour Is Too Important to Leave to Chance
Print will always be the part of the garment people see first.
But the sum of all parts — the fabric, the trims, the fasteners, the finish — is what determines whether a design actually delivers on its promise. Brands that continue to treat colour as a single creative decision, rather than a coordinated technical discipline spanning their entire supply chain, will keep paying for it in re-dips, delays, and disappointed design teams.
A Century of Textiles, and an Ever-changing World
Few companies can trace their roots back more than a century and still count themselves among their industry's innovators. Texia, headquartered in Monistrol de Montserrat, Spain, is one of them.
But the story of Texia is not simply one of longevity.
It is a story of continual reinvention. As the textile industry has grown more global and competitive, Texia has repeatedly reshaped its business, investing in technology, developing its own brands, and placing sustainability at the centre of its mission. In doing so, it offers a compelling example of how a heritage manufacturer can lead rather than follow through a period of profound industry change. Image Credit: Texia
What are we craving Ultimately?
The instinct to slow down while simultaneously optimising every measurable aspect of life isn't a passing curiosity. It's a structural response to a world that feels increasingly unstable, and it's reshaping what people expect from their homes, hotels, workplaces and healthcare environments alike.
For the design and manufacturing sectors, this means rethinking both product and process.
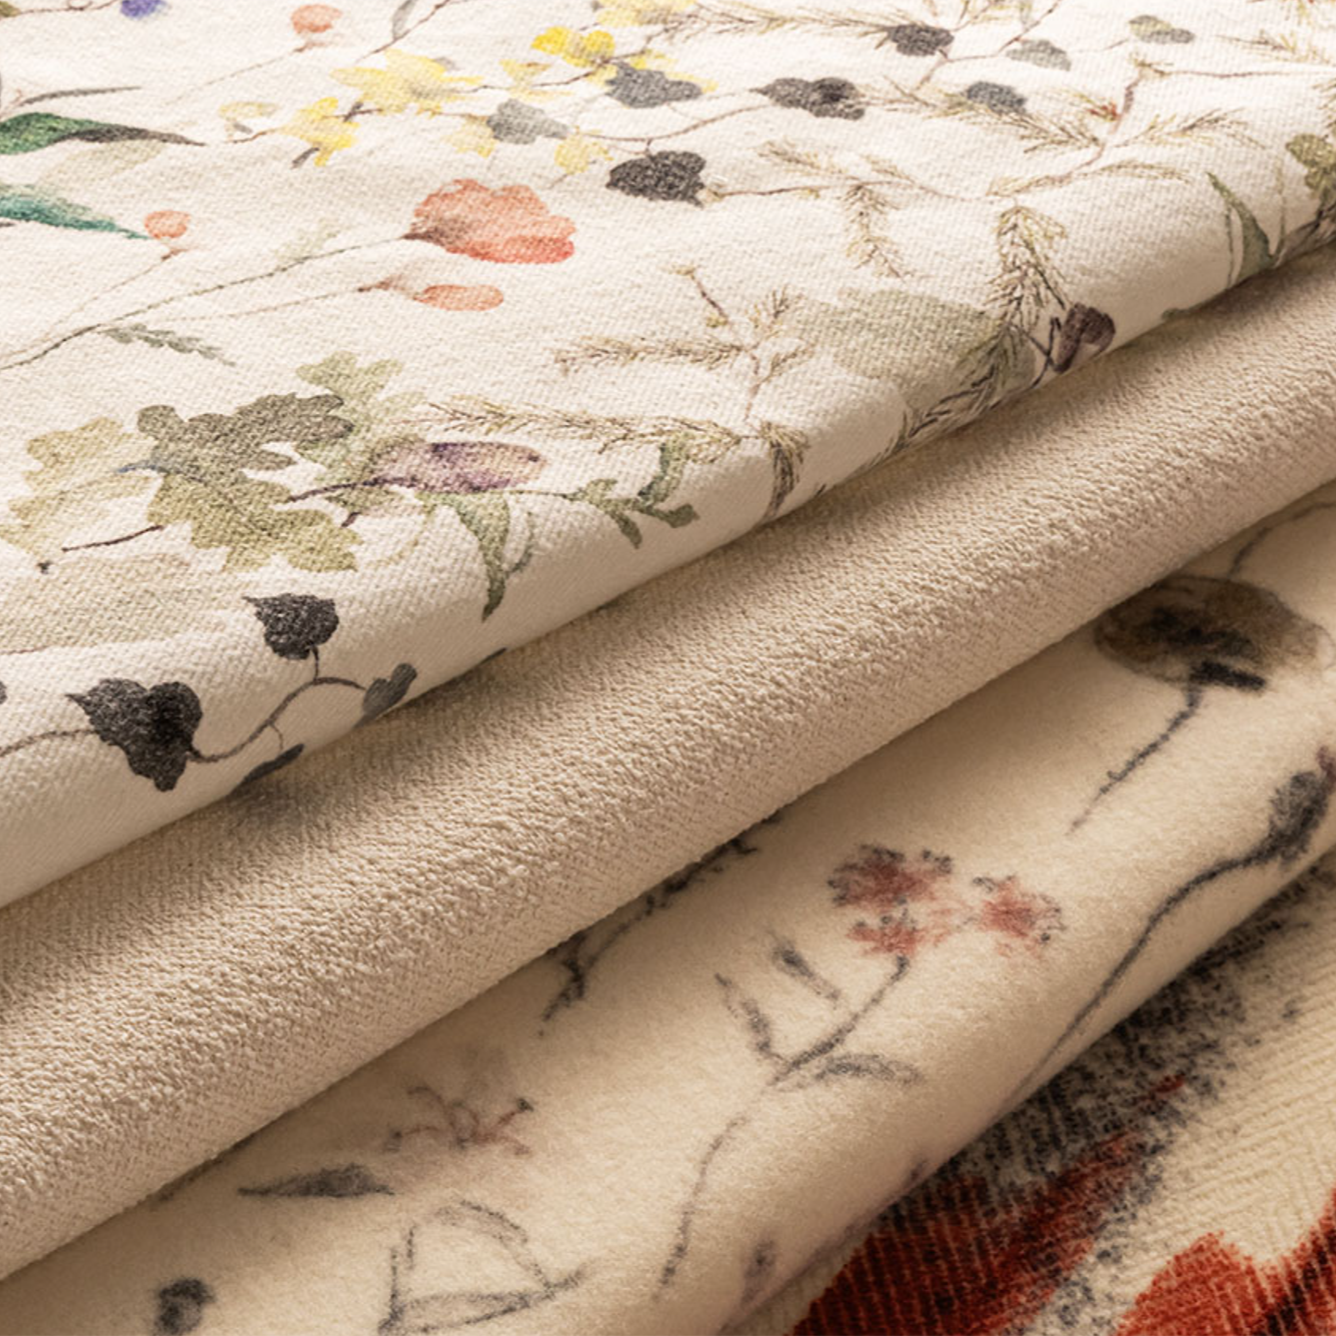
The Structual Shift is Real and its Already Here
Volumes are moving east, where digital production is accelerating rapidly. Consumer behaviour has shifted.
Demand is now driven by personalisation, shorter buying cycles, and an expectation of near-instant responsiveness. Regulatory pressure is intensifying, with supply chain transparency now a legal and commercial fact in many markets. And margins? They are under sustained, structural pressure.
This is not a temporary disruption. It is a fundamental reordering of how textile manufacturing must operate.
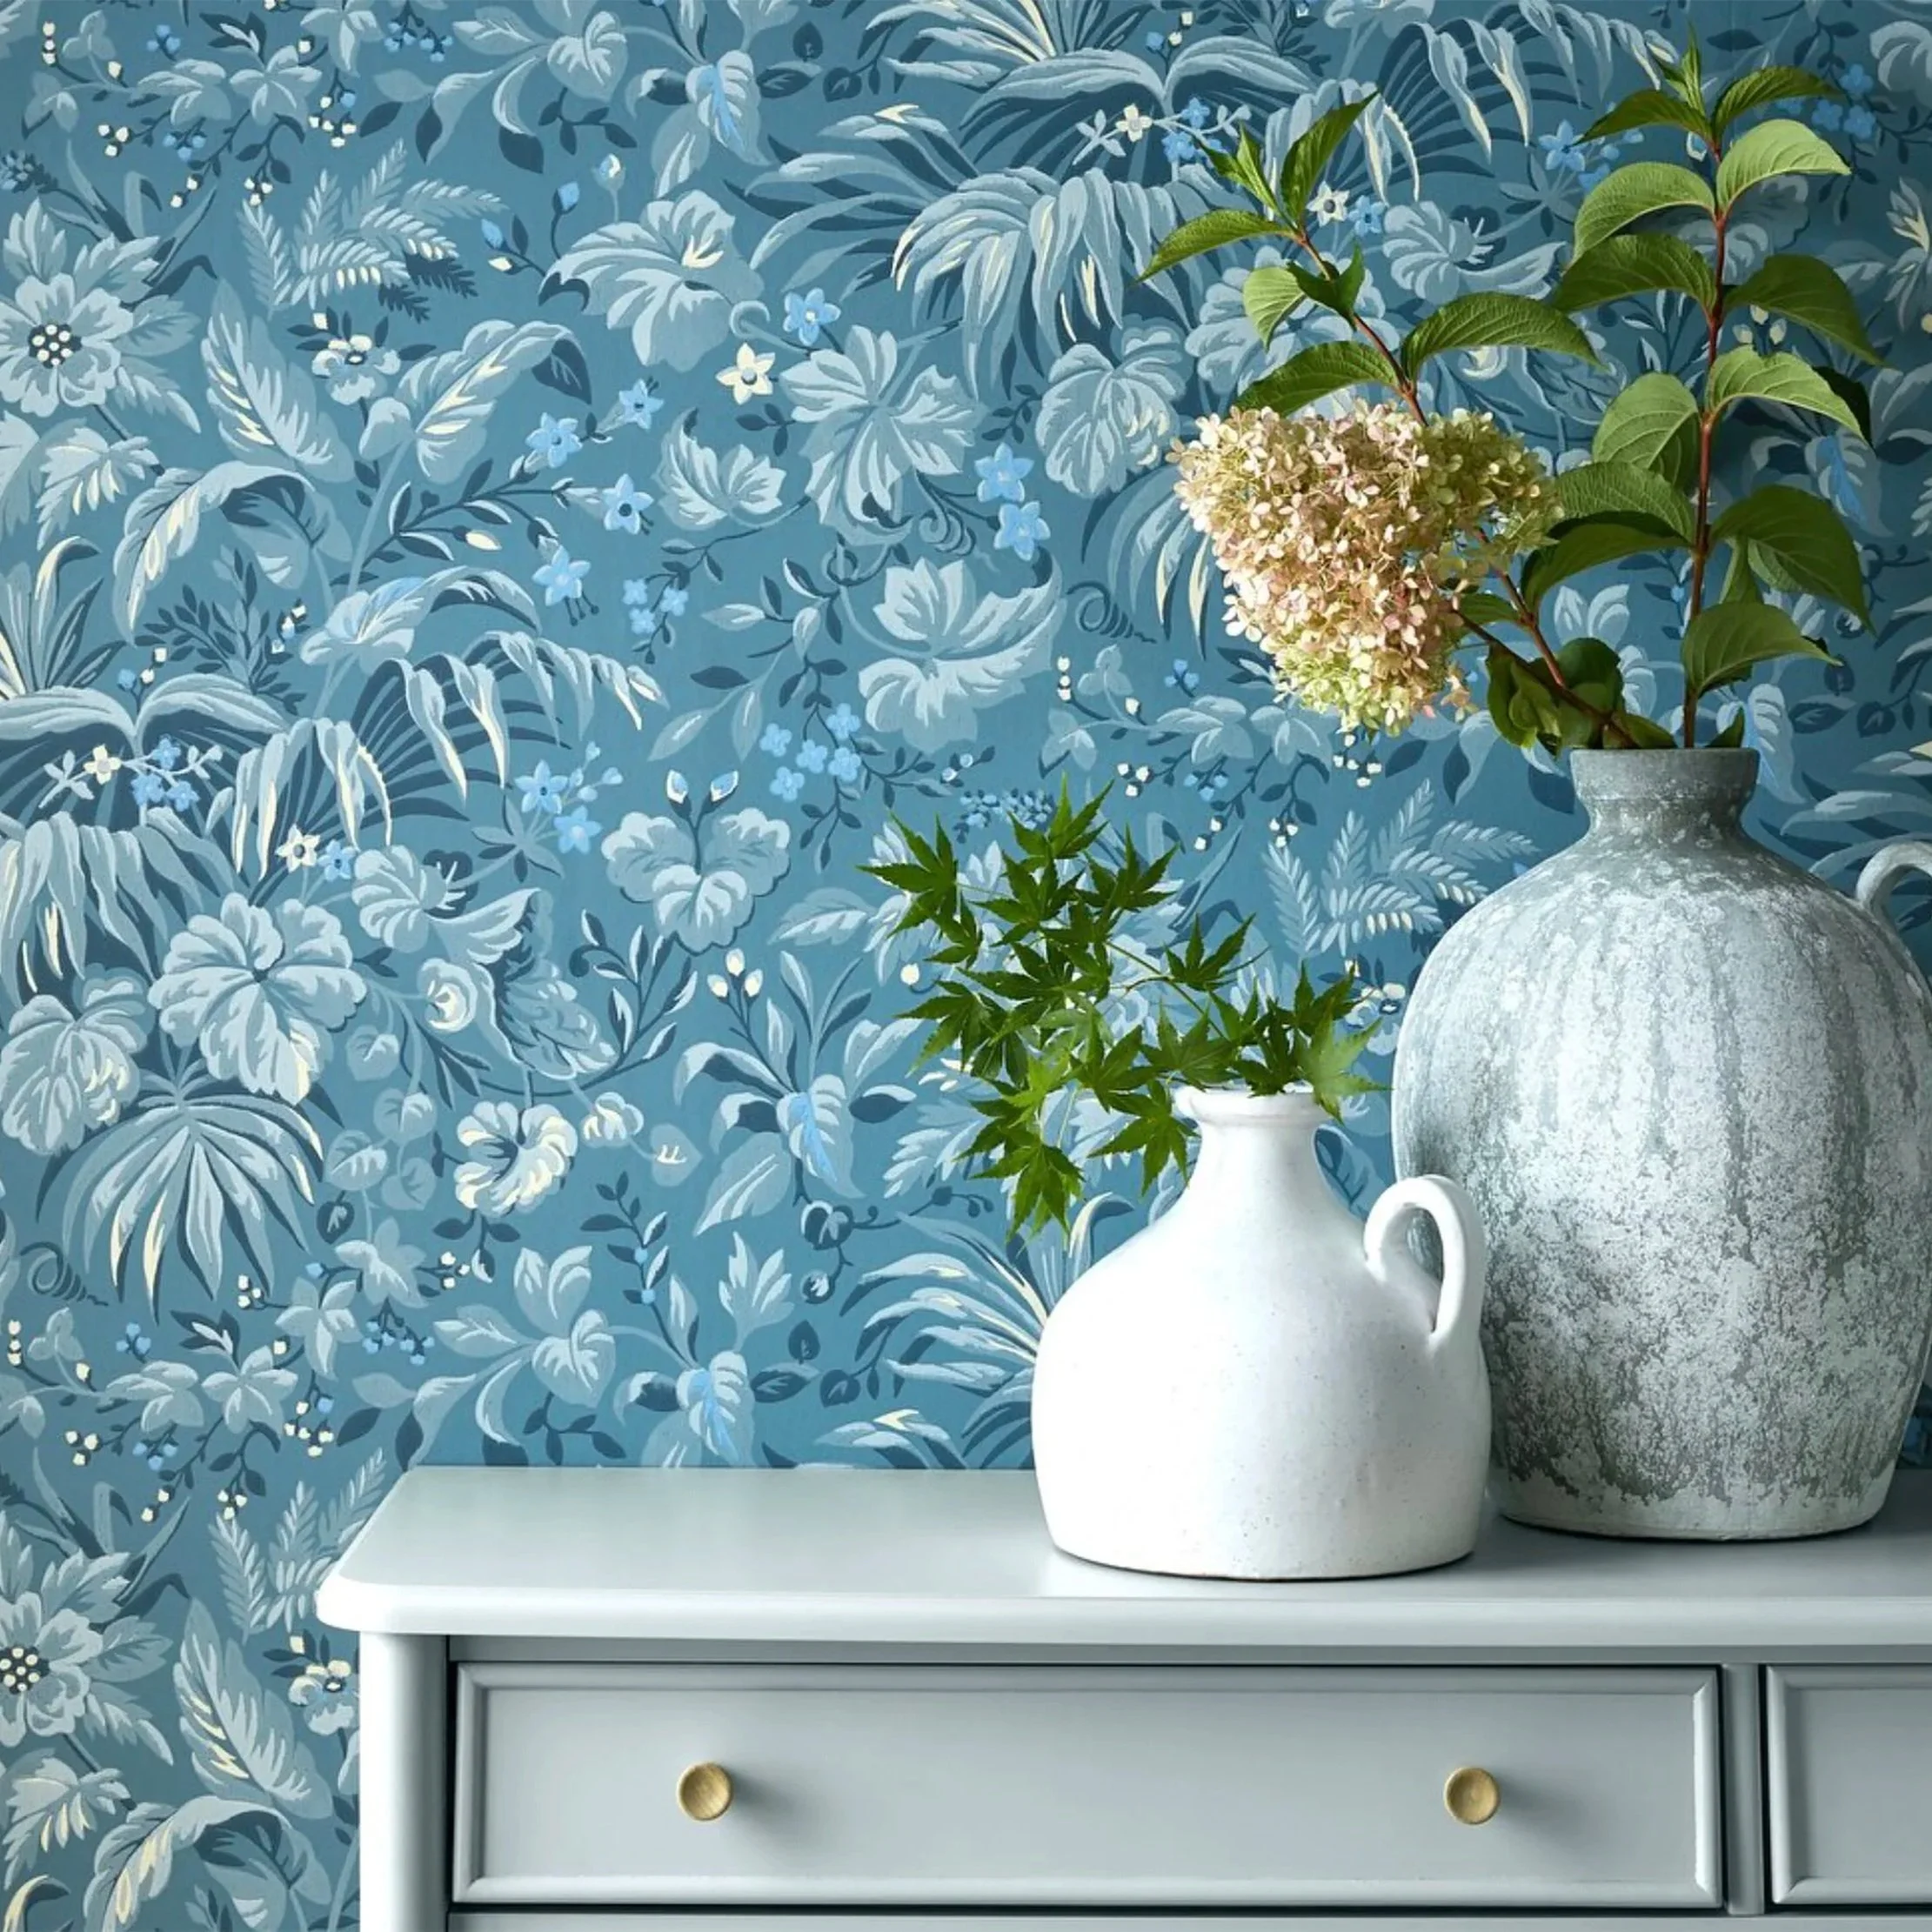
The Challenge: Standing Firm as the Industry Shifts
The wallpaper landscape has changed dramatically. Digital printing has lowered the barrier to entry, spawning countless direct-to-consumer brands and pushing much of the market towards faster, cheaper production.
At the same time, manufacturing in the UK has grown steadily harder - rising minimum wage, national insurance, energy and substrate costs all bear down on margins. Surface Print have embraced all of these challenges - and stand resolutely prepared for the future.
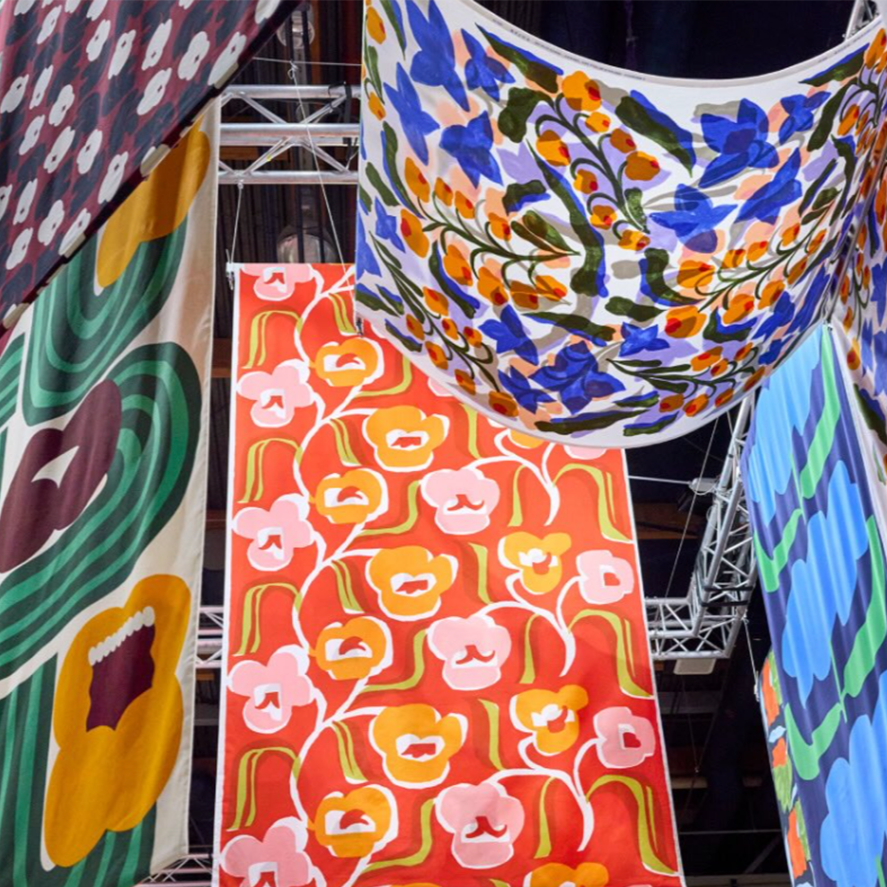
From Helsinki's printing mill to Paris's Le Marais, discover how Marimekko is scaling a design-led brand with purpose, craft, and bold innovation.
But what makes Marimekko's story compelling is not just its aesthetic legacy?
The word "toxic" carries weight. It conjures danger, harm, and things best avoided.
“Yet in the textile industry - Where between 3,000 and 10,000 chemicals move through the supply chain, a reflexive fear of the term is one of our biggest obstacles to progress.”
This article distils the key takeaways and what buyers, designers, and brands should be asking right now.
What Is the Digital Product Passport?
At its core, a Digital Product Passport is a digital record attached to a physical product - For a printed textile product, this means the DPP would capture data on the substrate, inks and dyes used, the printing process and technology, chemical compliance, environmental impact (including water and energy use), supply chain traceability, and end-of-life instructions.
The Market Gap that Changed Everything
Future Fashion was founded in 2019, timed deliberately to coincide with a pivotal moment in global textile technology: the commercial launch of the EFI Reggiani BOLT Single-Pass digital printing system.
The founders recognised that single-pass architecture had fundamentally changed what was industrially possible - and that Pakistan's domestic market had yet to catch up.
Print is no longer defined by the inefficiencies that once characterised it…as advances in production processes and technology have significantly improved its environmental performance.
Taran Rai, Corporate Sustainability Manager at Epson explains why?
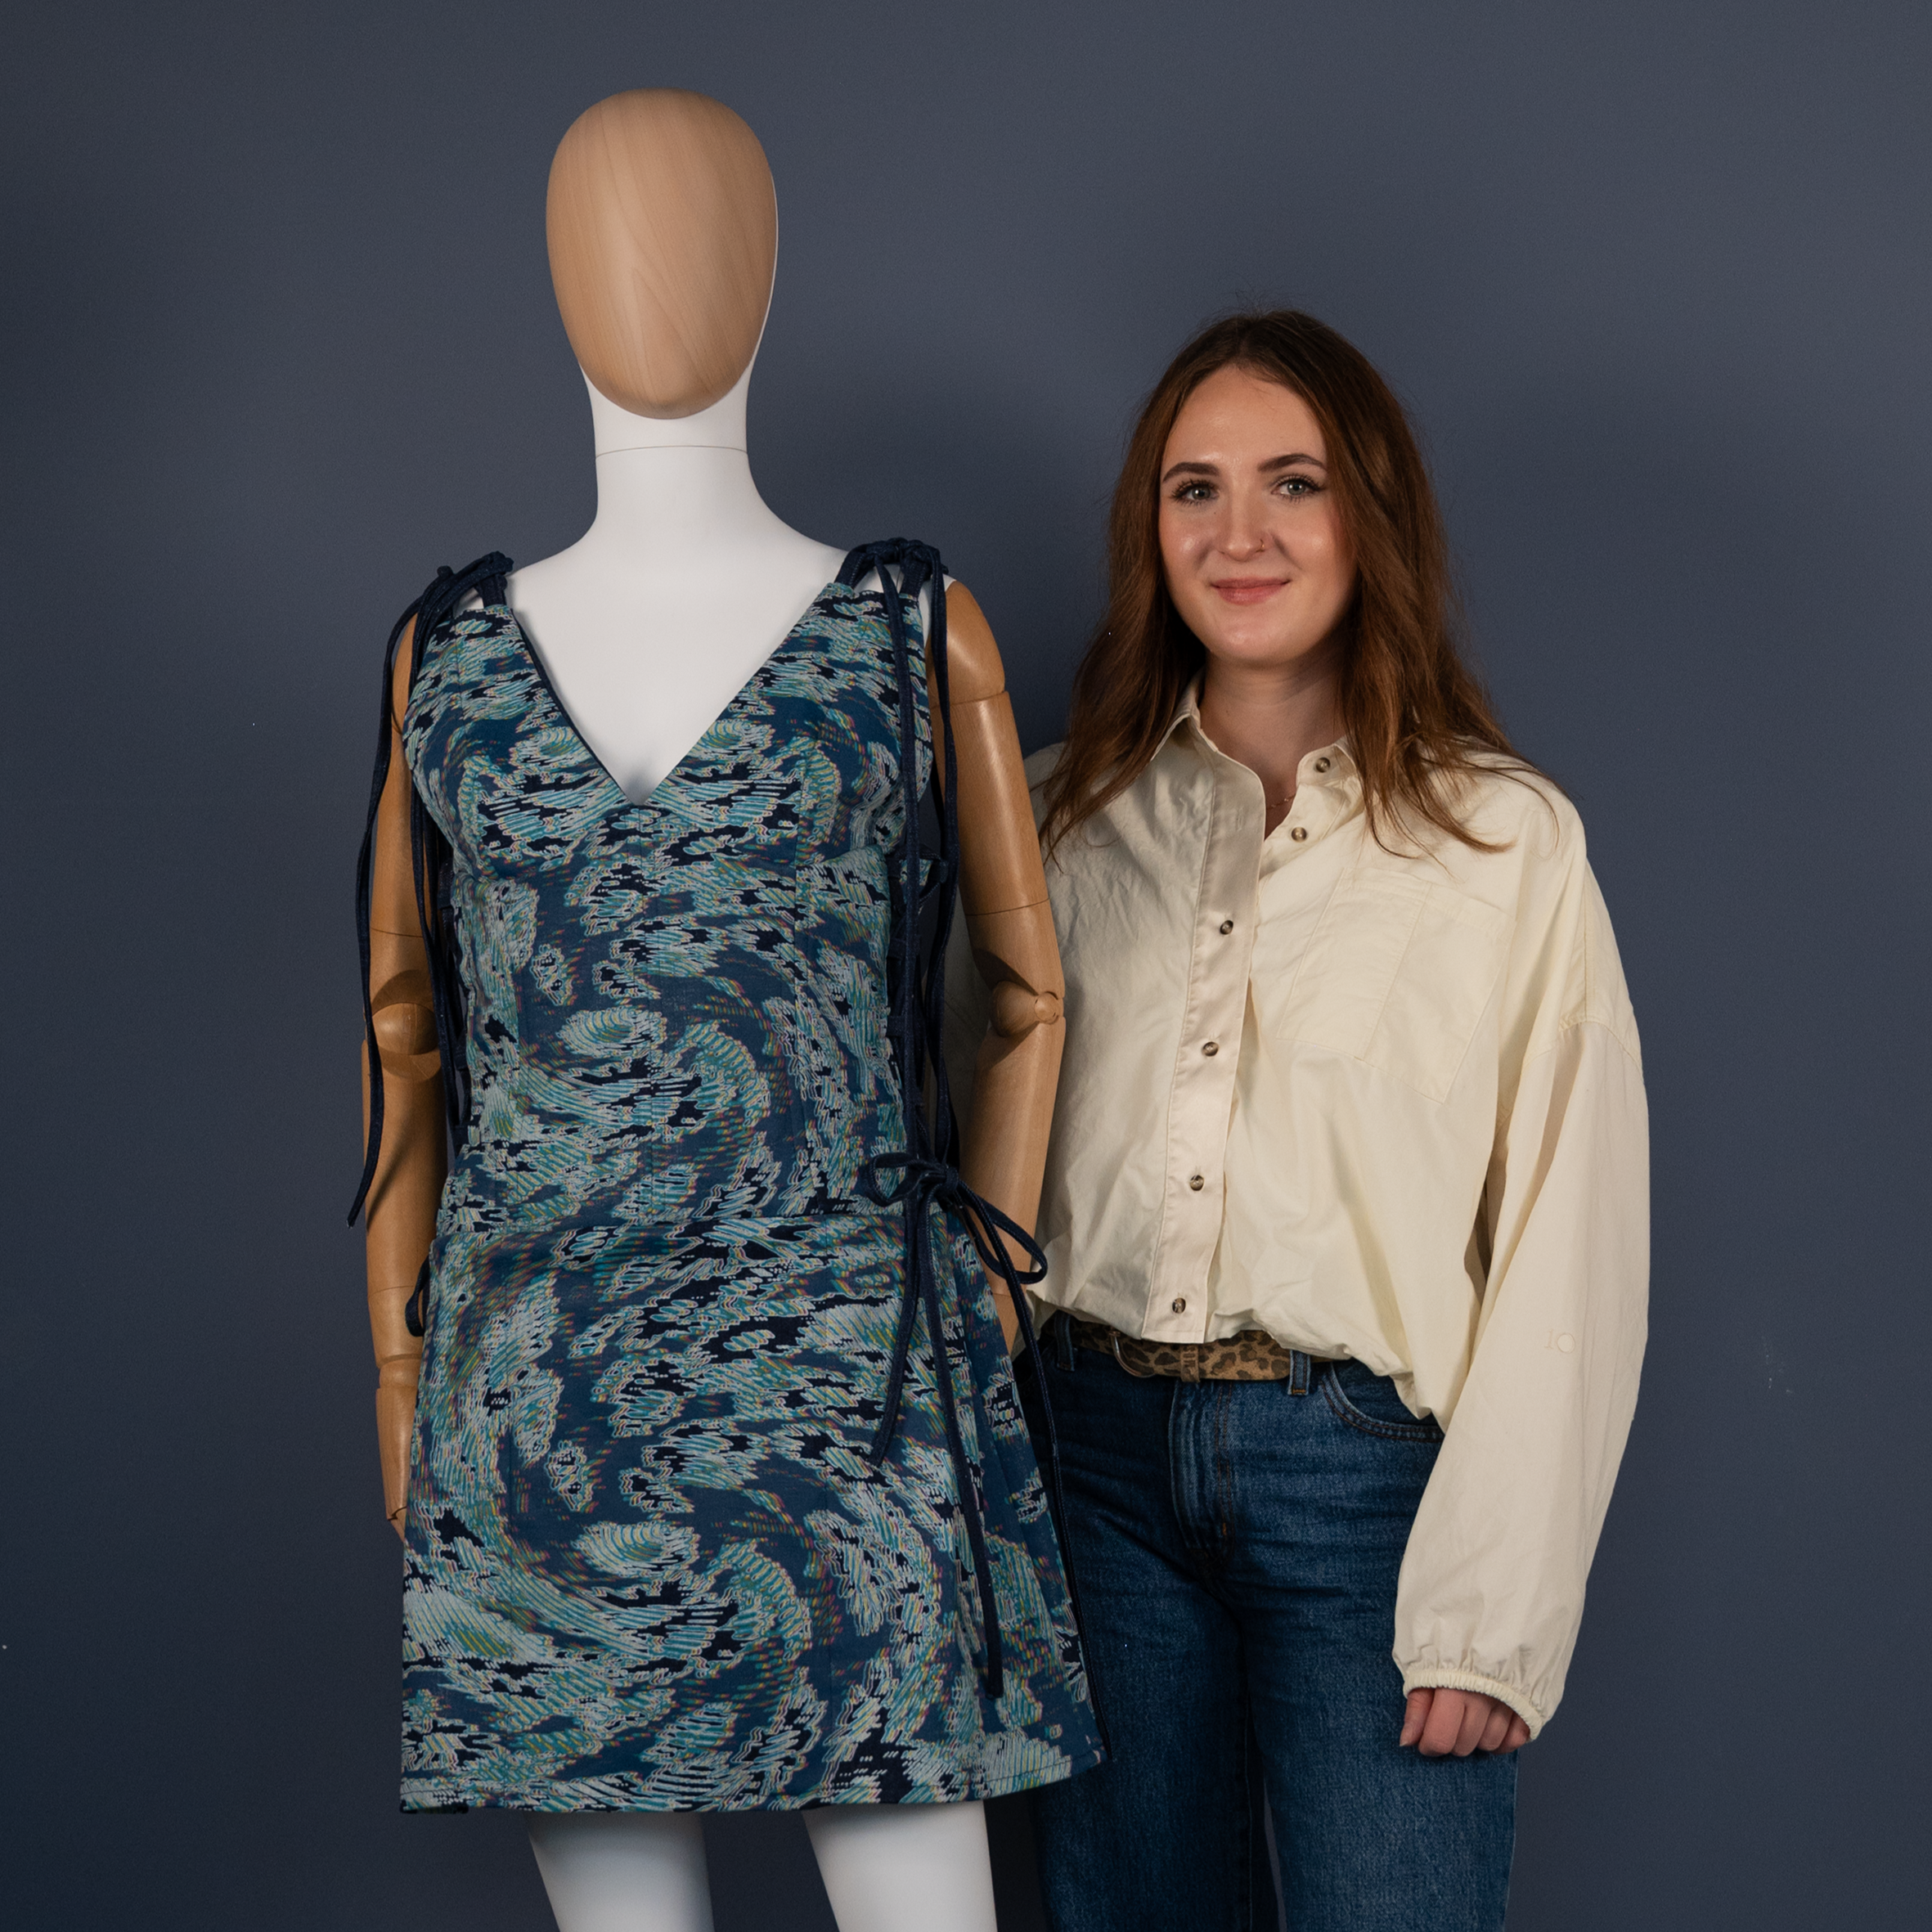
The story of what happens when young designers access digital technology is still being written.
What once was a theoretical sustainability goal seems to have shifted into an active regulatory reality.

Is the Textile Market Finally Recovering?
After a difficult few years, there are genuine reasons for optimism. Duncan was candid about the challenges: "The market for textiles has been very difficult over the last three years. I'm not going to hide the truth there. But the tide is turning.“
A profound shift is currently reshaping the sector
Changing consumer expectations demand greater design diversity, faster turnaround times, and sustainable manufacturing practices.
To thrive, interior brands must adapt their supply chains, bringing production closer to the end consumer and moving away from bulk manufacturing.
Digital textile printing offers a definitive solution to these operational bottlenecks.
Digital transformation doesn't announce itself.
It accumulates - one innovation at a time - until an entire industry looks back and realises the ground has shifted beneath its feet. That's precisely where textiles stands today.
The conversations happening now about AI, automation, sustainability, and digital product passports are not theoretical. They are shaping decisions being made on factory floors and in boardrooms right now.
“By leveraging advanced digital textile printing, Marylene Madou has successfully merged traditional craftsmanship with cutting-edge technology. Her approach offers a blueprint for how independent designers can scale their brands globally while maintaining a minimal environmental footprint.”
The textile industry is undergoing a vital transformation. As the insights from Techtextil and Texprocess reveal, the path forward relies on a combination of sustainable hardware, intelligent chemistry, and seamless digital workflows.
From Zimmer's industrial-scale energy reductions and Stratasys's on-demand 3D embellishments, to Kornit's single-step technical printing and the unified digital ecosystems of NedGraphics and Optitex, the tools for change are here. To stay competitive, brands and manufacturers must adopt these innovations, moving away from fragmented, wasteful processes towards a truly connected, circular economy.
Friedmans stands as a testament to the power of combining traditional textile knowledge with forward-thinking innovation.
“Operating from their UK headquarters, Friedmans now serves a diverse array of sectors, including swimwear, dance, entertainment, sportswear, interior decor, prosthetics, and even pet apparel. With a strategic supply chain that reliably serves clients worldwide”
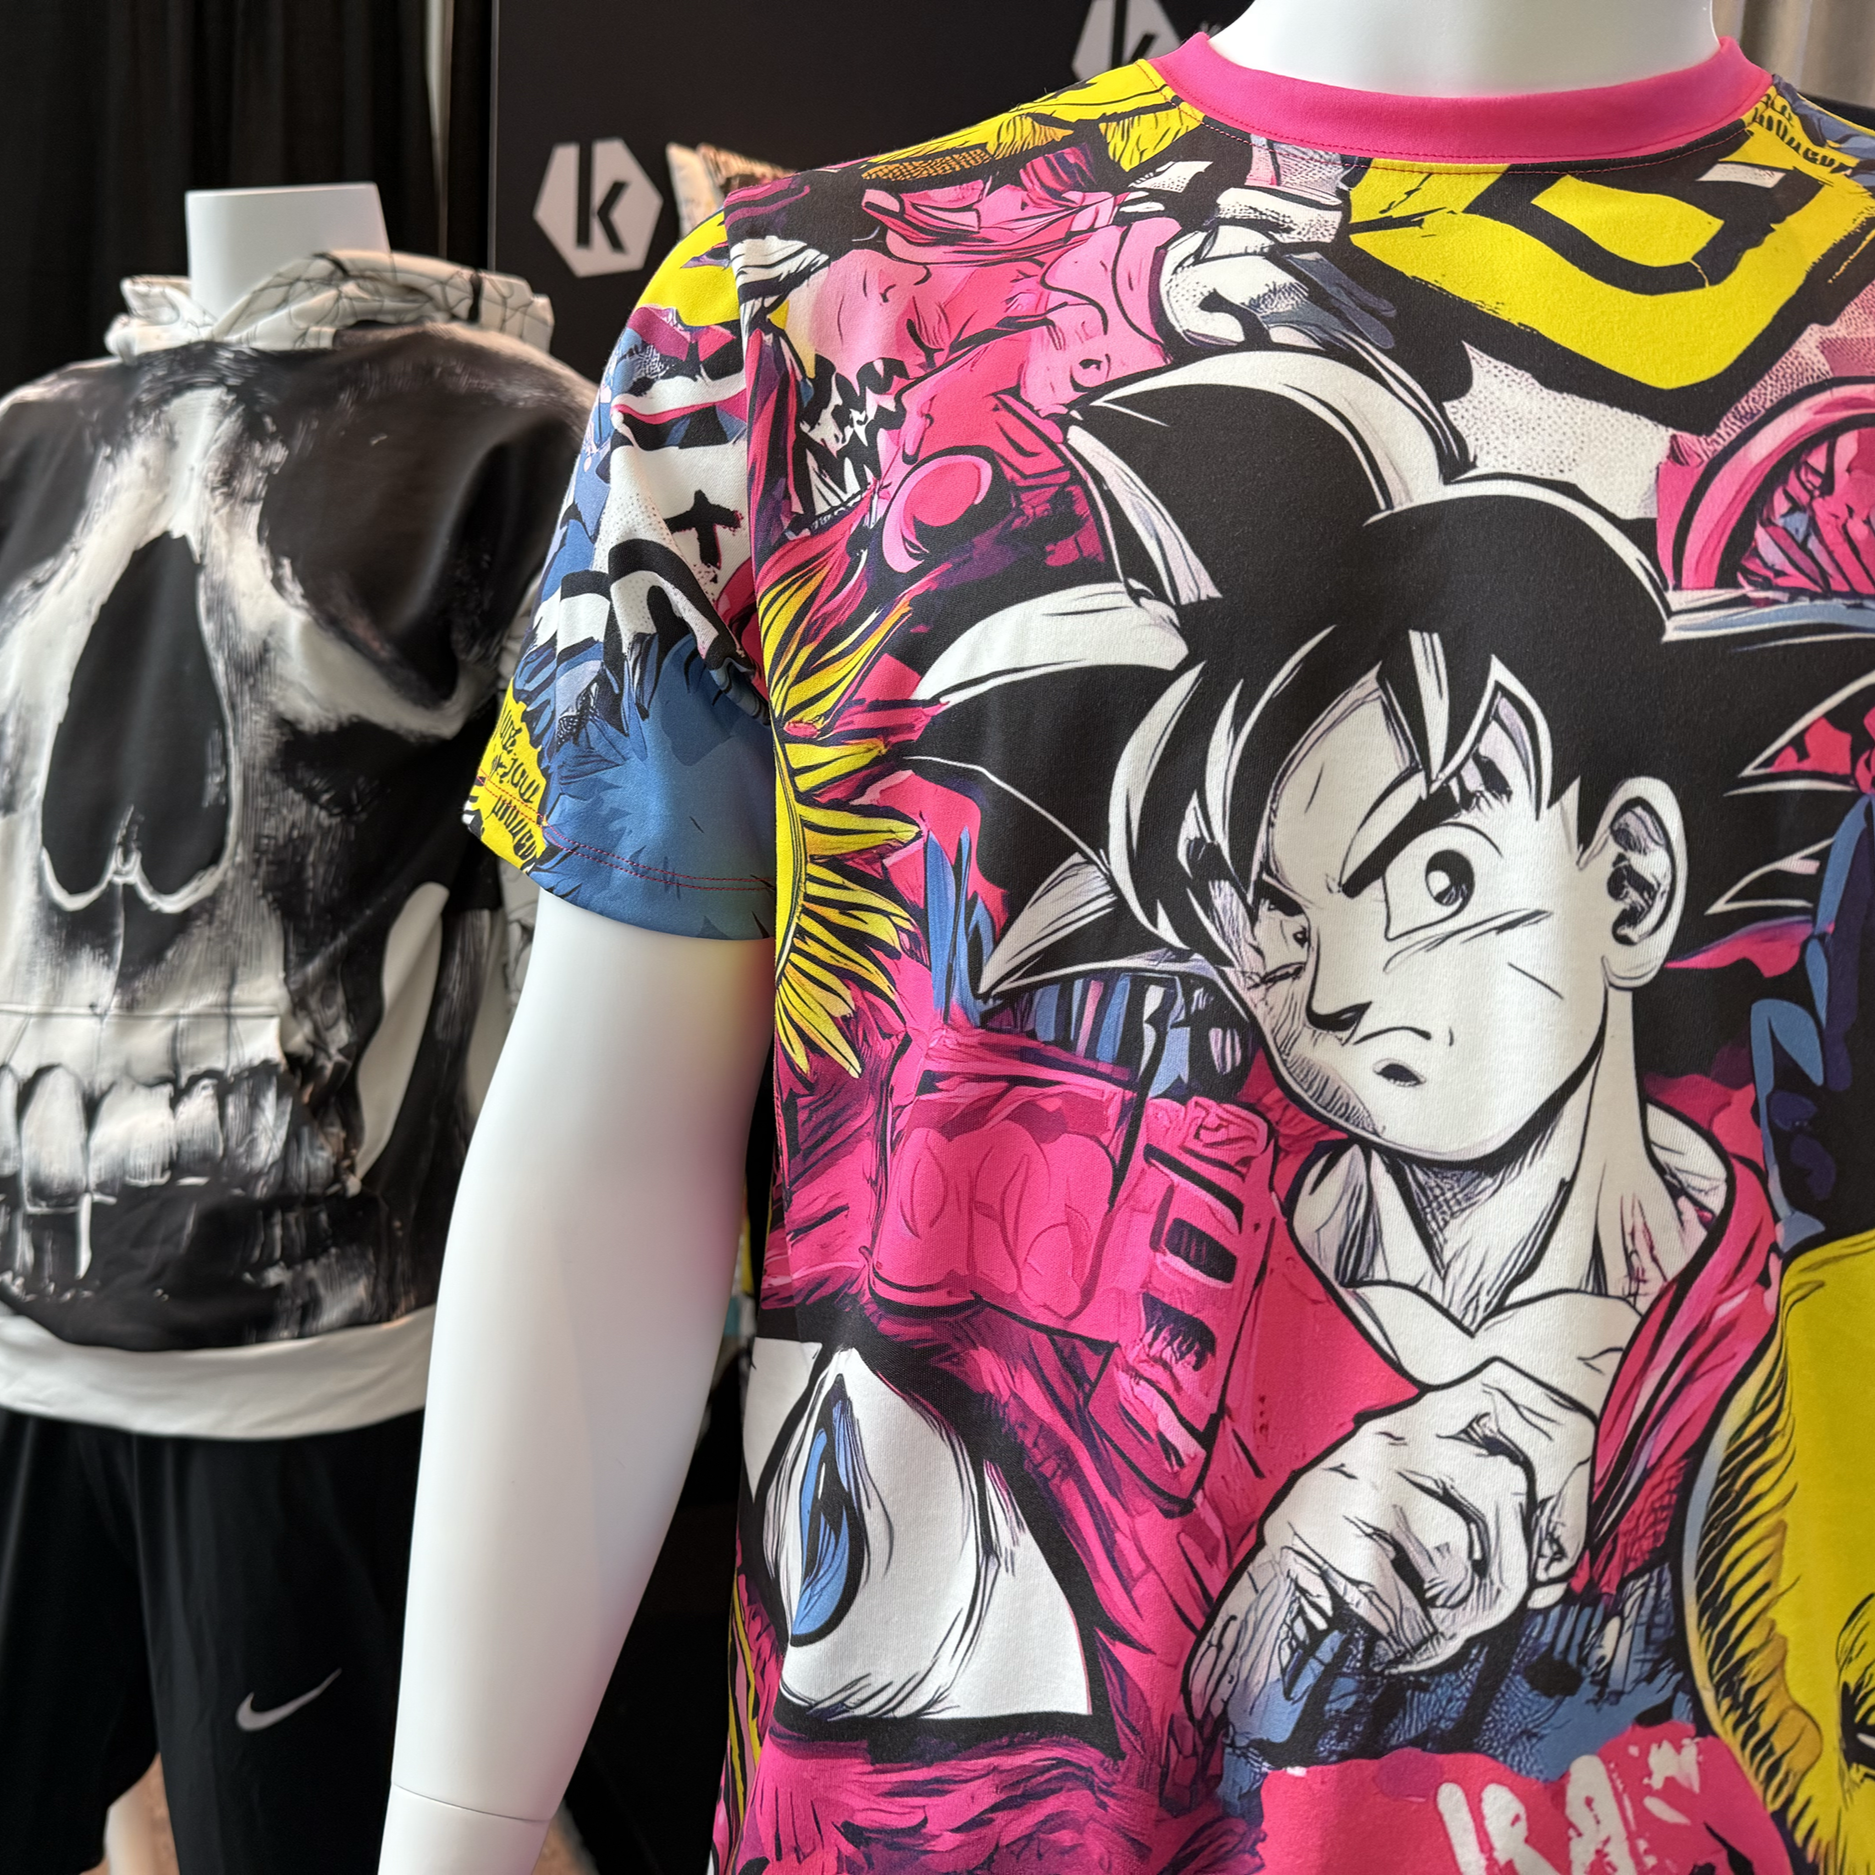
The apparel decoration industry is decisively moving away from isolated, analogue production tools toward connected digital manufacturing environments.
"Kornit’s unwavering commitment to transformative technology continues to disrupt the status quo. For business leaders and innovators ready to capture the future of apparel manufacturing, the path forward is clear”
The Urgent Need for Sustainability at Scale
The transformation at Coats provides a vital blueprint for the wider textile and apparel sector. True sustainability cannot be achieved in silos. As Dearing emphasised:
“Cross-industry collaboration is the engine of meaningful change. Brands, machinery suppliers, chemical providers, and fibre producers must act as an interconnected ecosystem”
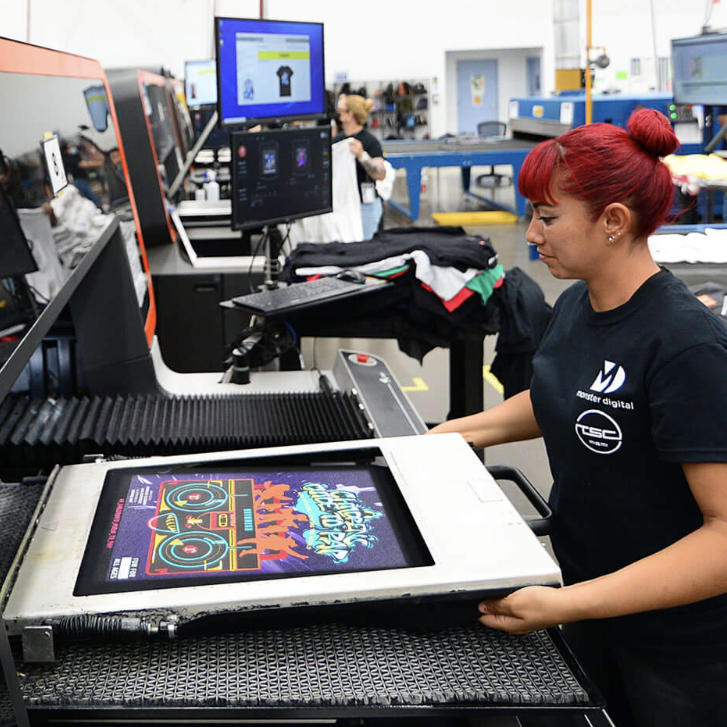
Today’s customers demand superior product quality, real-time data visibility, and lightning-fast turnaround times.
For large-scale garment decorators, managing these expectations while balancing seasonal demand fluctuations - such as the massive surges seen during Black Friday - presents a monumental challenge.
"Relying on transactional vendor relationships and outdated legacy equipment is no longer sufficient to secure long-term stability and growth.”
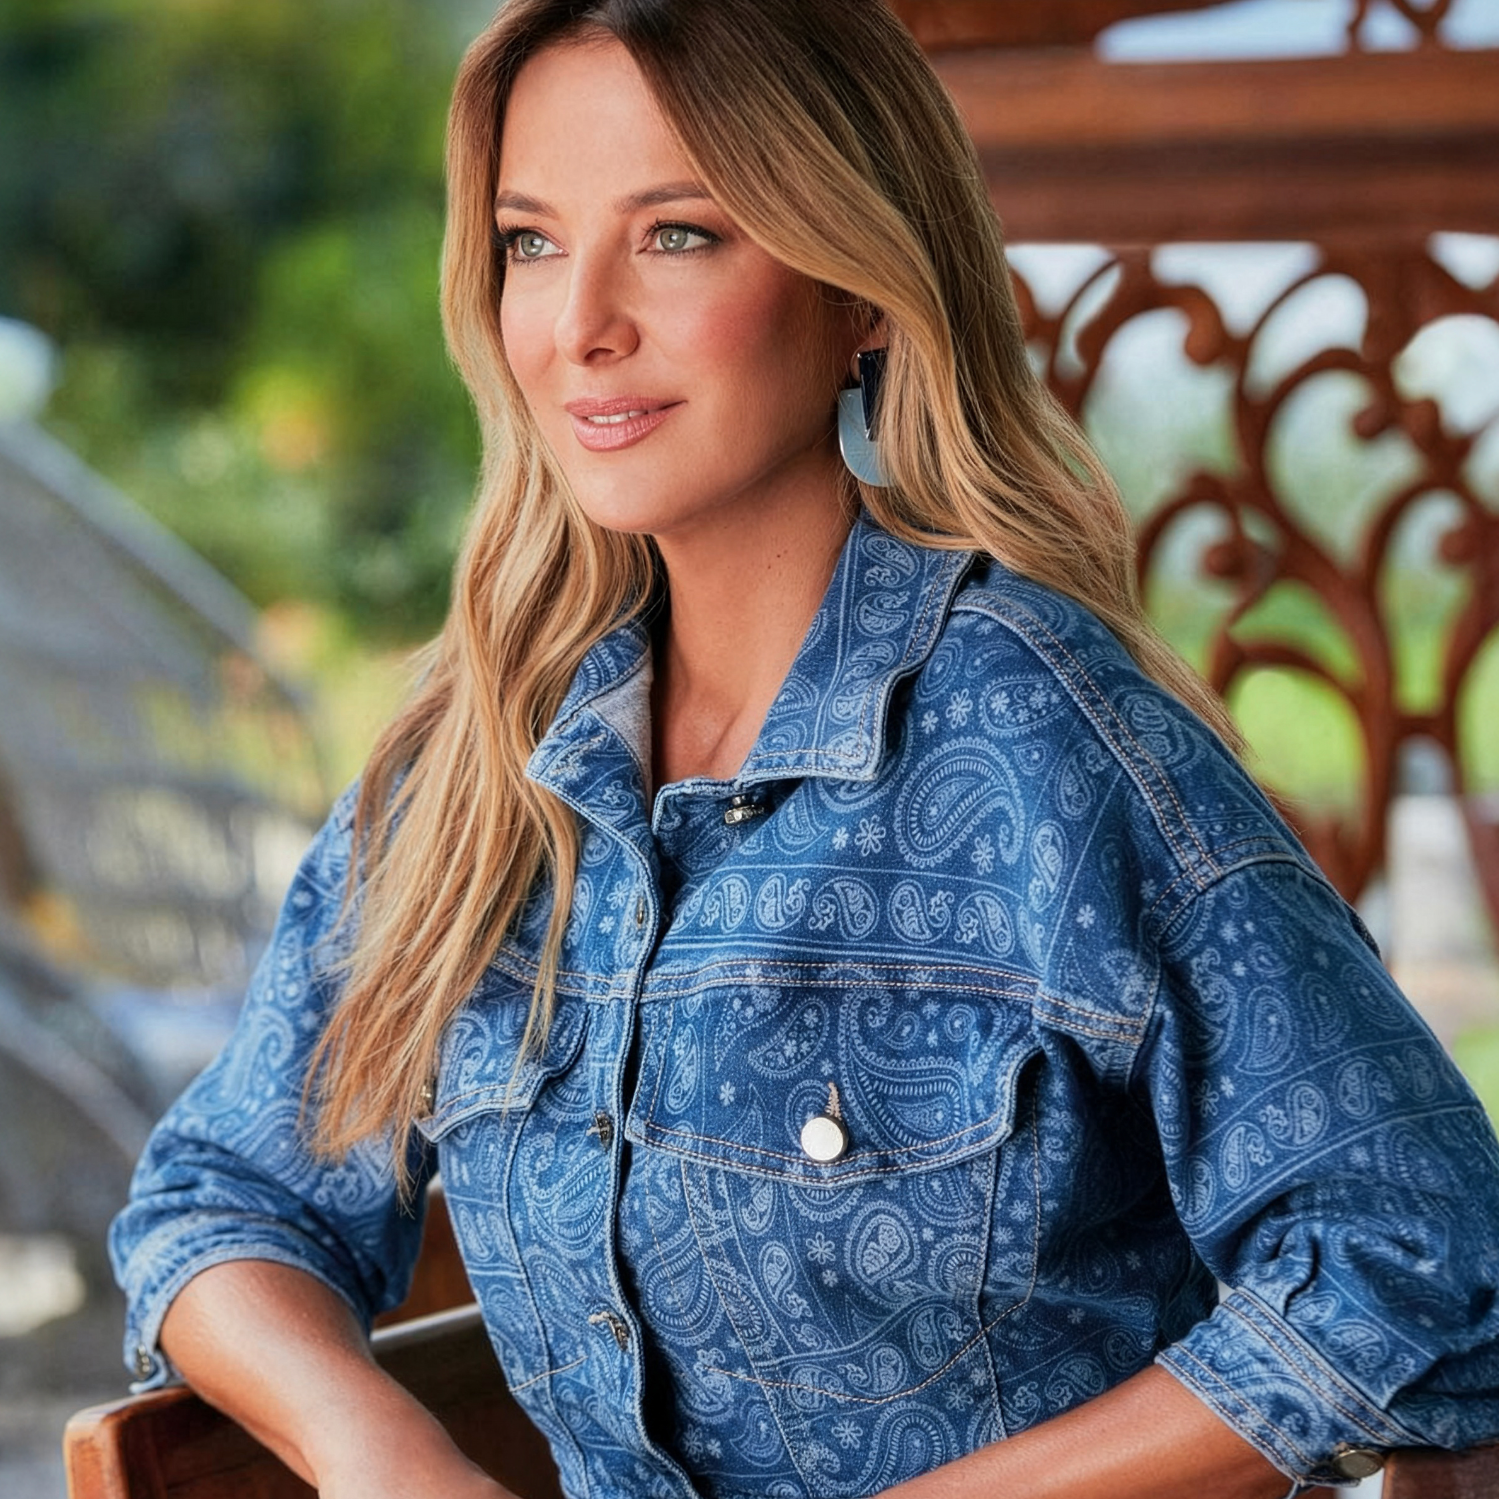
Printing method is never a secondary detail. It shapes the entire life cycle of a product, from concept to customer. In today’s fashion industry, where margins are tighter and speed matters more than ever, technical knowledge has become a competitive advantage.
“The future of textile design belongs to professionals who can combine creativity with execution, aesthetics with practicality, and vision with production reality”.
Durst develops and markets advanced solutions for digital production, automation, and intelligent manufacturing across industrial applications worldwide.
Roland inkjet printers and printer/cutters are widely used in a variety of visual communication fields, including signage and interior decoration.

The leading manufacturer of digital and screen-printing machinery, coating, steaming and drying systems for textile and carpet processing

EFI Reggiani has become the trusted partner for integrated, scalable solutions for the entire textile process – from yarn treatment to fabric printing and finishing.

Epson industrial digital workflow for textile printing, from technology to inks, from pre- to post-treatment and learn about Epson Textile Solution Center.

Resolute isn't just a DTF printer and supply company, they are innovators in the field, shaping the future of textile decoration with innovative DTF solutions.

As the exclusive UK & Ireland distributor for Mimaki Engineering; its industry-leading product range that comprises solvent, LED UV, 3D, dye sublimation and textile inkjet printers, cutters, inks, software.
At Agfa, we believe in print as an essential and powerful medium of communication. Our mission is to enable printing businesses to achieve profitable growth.

Brother has a comprehensive range of solutions in the areas of direct-to-garment printing - from mass production to smaller printers for customisation.

VeriVide are the light and colour experts. UK based but global specialist in the design, development and manufacture of standardised lighting cabinets & digital imaging systems (DigiEye).

Since 1986, our aim has always been the same, to add value beyond print - to create cutting-edge laminating and print finishing equipment of the highest quality.

Kornit’s innovative printing technology enables businesses to succeed in web-to-print, on-demand and mass customization concepts.

Imagine a production process where 2D sewing and cutting happen in one seamless, automated operation - no manual handling required.

Award winning supplier wide range of Printers, Finishing Equipment, Inks & Media, RIP & Colour Management Solutions and Warranty & Service Support.

Soyang Hardware offers leading edge wide and superwide format print production hardware solutions from many of the industry’s biggest and best-known printer brands..

Klieverik is a leading manufacturer of rotary thermo-processing equipment, specialising in advanced textile applications.

With Barbieri, digital textile printers achieve professional ICC profiling, calibration, and quality control - leading to enhanced color consistency and confidence across all materials.
At China Print Supplies Ltd, we are more than just a distributor - we are your strategic partner in print solutions. With a commitment to excellence and a passion for innovation

A key supplier of dye-sublimation printing equipment, consumables, and support services to a diverse range of customers across the United Kingdom.